- English
- French
- German
- Portuguese
- Spanish
- Russian
- Japanese
- Korean
- Arabic
- Irish
- Greek
- Turkish
- Italian
- Danish
- Romanian
- Indonesian
- Czech
- Afrikaans
- Swedish
- Polish
- Basque
- Catalan
- Esperanto
- Hindi
- Lao
- Albanian
- Amharic
- Armenian
- Azerbaijani
- Belarusian
- Bengali
- Bosnian
- Bulgarian
- Cebuano
- Chichewa
- Corsican
- Croatian
- Dutch
- Estonian
- Filipino
- Finnish
- Frisian
- Galician
- Georgian
- Gujarati
- Haitian
- Hausa
- Hawaiian
- Hebrew
- Hmong
- Hungarian
- Icelandic
- Igbo
- Javanese
- Kannada
- Kazakh
- Khmer
- Kurdish
- Kyrgyz
- Latin
- Latvian
- Lithuanian
- Luxembou..
- Macedonian
- Malagasy
- Malay
- Malayalam
- Maltese
- Maori
- Marathi
- Mongolian
- Burmese
- Nepali
- Norwegian
- Pashto
- Persian
- Punjabi
- Serbian
- Sesotho
- Sinhala
- Slovak
- Slovenian
- Somali
- Samoan
- Scots Gaelic
- Shona
- Sindhi
- Sundanese
- Swahili
- Tajik
- Tamil
- Telugu
- Thai
- Ukrainian
- Urdu
- Uzbek
- Vietnamese
- Welsh
- Xhosa
- Yiddish
- Yoruba
- Zulu
What is a double deck roll forming machine and when to buy one?
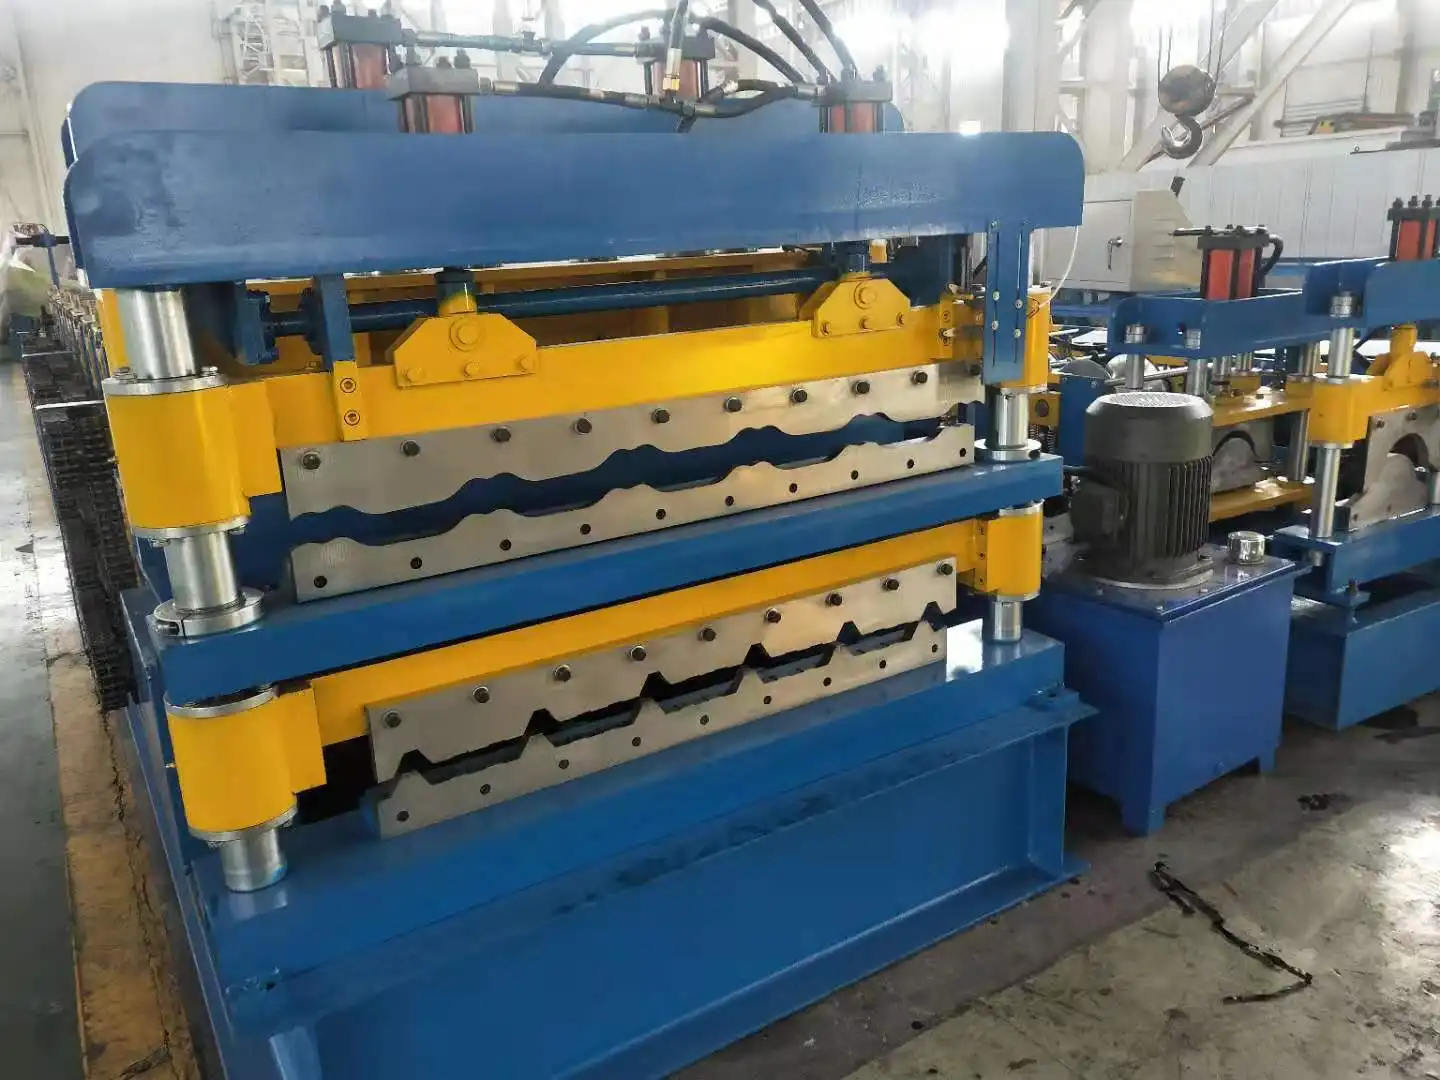
A double deck roll forming machine is a specialized cold-forming system that houses two complete profile tooling sets within a single integrated frame, allowing operators to switch between two distinct deck profiles without retooling downtime. Unlike a conventional single-profile line, this configuration effectively doubles usable output capacity inside the same floor footprint. For deck manufacturers, steel-building contractors, and composite-slab subcontractors serving the U.S. high-rise and industrial construction markets, this dual-tooling architecture translates directly into schedule flexibility and faster tender fulfillment.
What Is a Double Deck Roll Forming Machine? Dual-Layer Architecture and How It Works
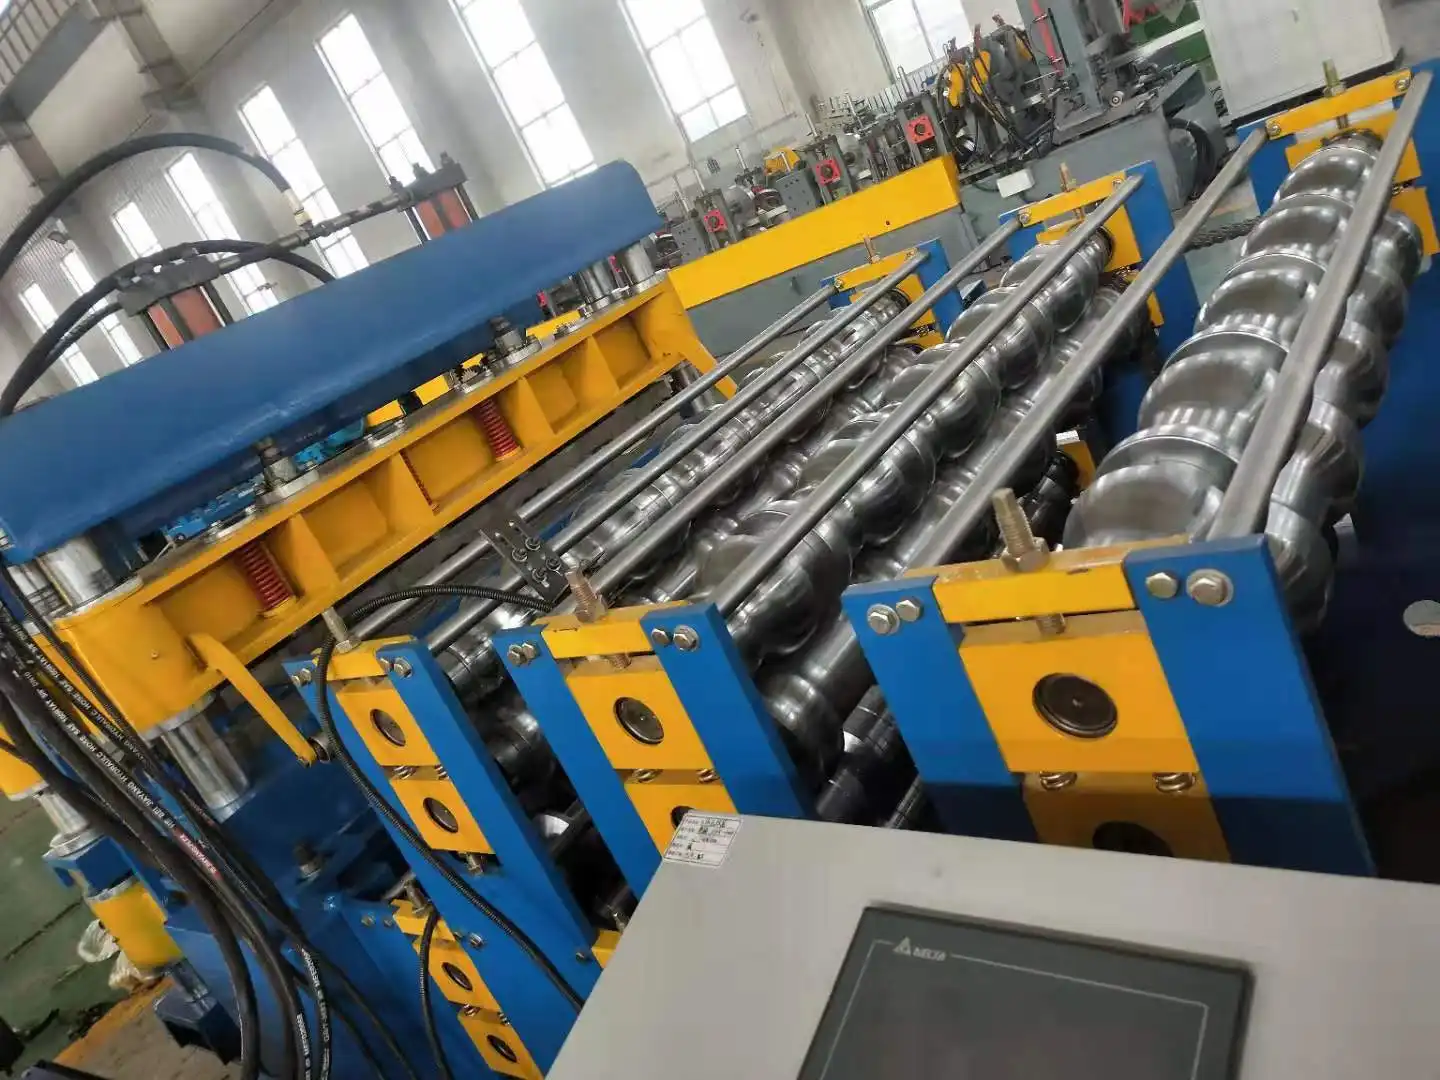
The machine moves galvanized or Galvalume coil stock, which is usually 0.8 to 1.2 mm thick and has a yield strength of 235 MPa, through a set of forming stations in a certain order. At each station, the strip is bent a little at a time until it reaches the final rib shape. Two full roller sets are stacked vertically on top of each other on the same base frame in a double-deck roll forming machine design. The operator uses the PLC console to choose which tooling deck to use, and then the corresponding roller train starts moving. Between profile runs, there is no need to switch coils or tools.
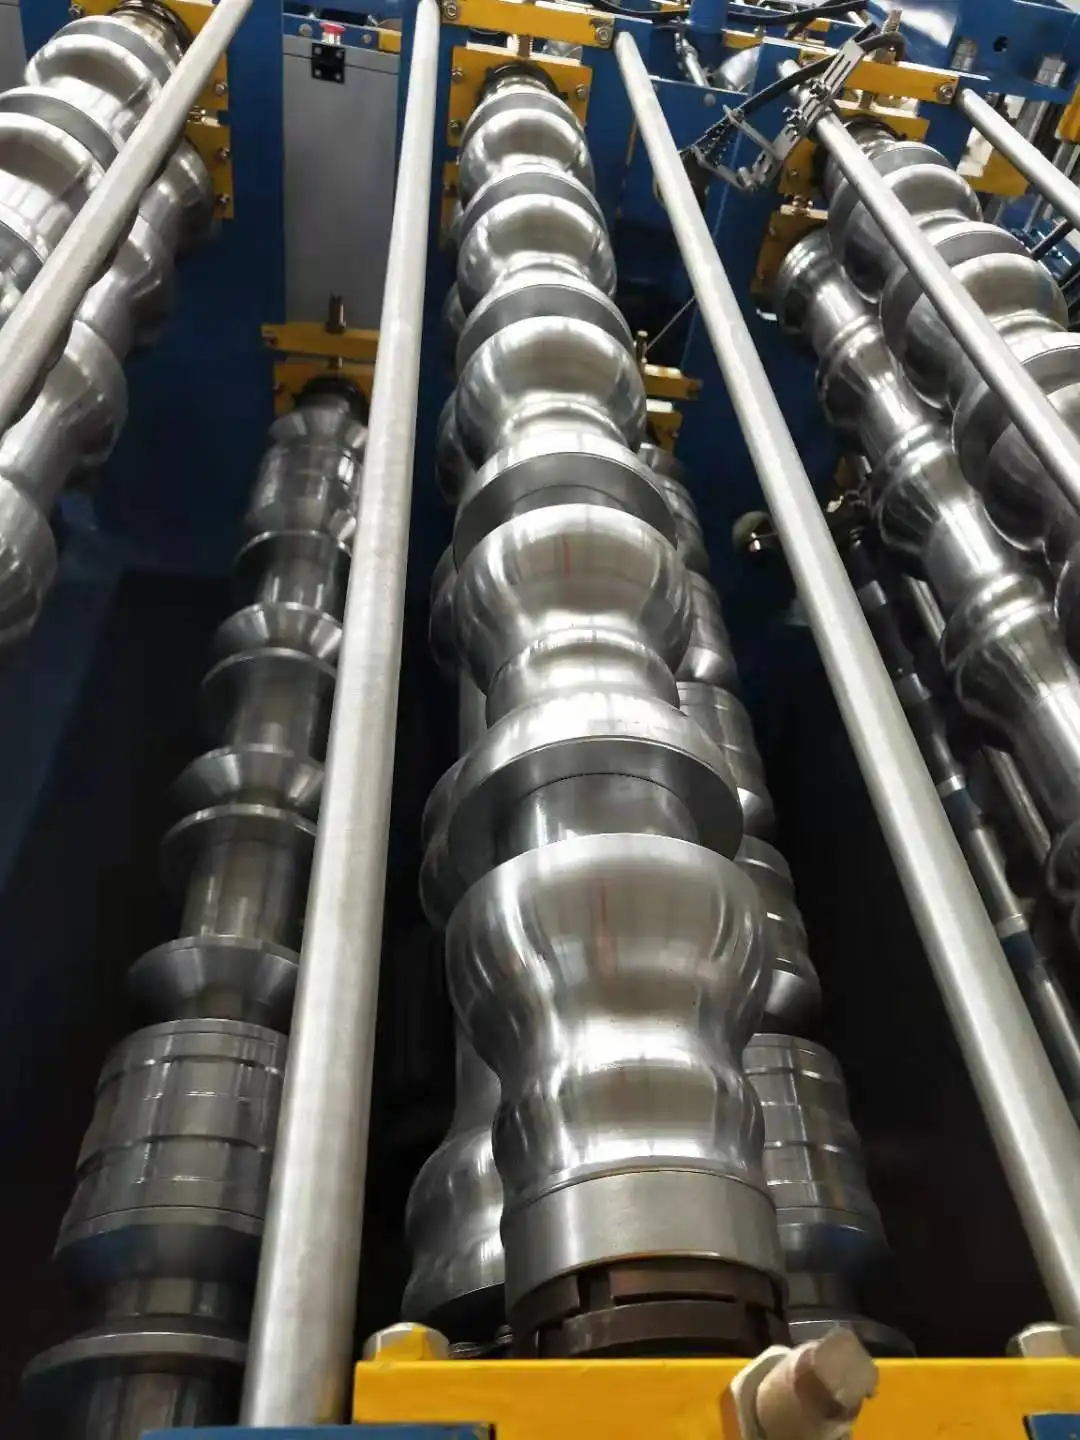
Forming roller shafts are 95 mm in diameter and are made from No. 45 steel that has been machined and given a chrome finish to protect them from rough galvanized coatings that are rough. To handle the higher rotational loads that deep-knurl patterns put on the composite floor deck, the stamping shaft steps up to 120 mm. The hydraulic cut-off unit uses CR12 mold steel cutters that have been quench-hardened. This makes clean shear edges that meet the ASTM A1008 tolerance requirements that are popular in U.S. structural deck standards.
A PLC and converter system is at the heart of the control design. Three separate 11-kW main motors spread power evenly across the forming train, which keeps the shaft from bowing during heavier-gauge runs. There is a 5.5 kW hydraulic unit that drives the cut-off press. Line speed ranges from 10 to 20 m/min, depending on the depth of the ribs and the difficulty of the embossing.


Benefits and Applications of Double Deck Roll Forming Machines
Core Production Advantages Worth Knowing
Running two profiles on the same line is useful for a lot more than just making things easier. In active production settings, these are the main benefits this equipment brings:
- Profile flexibility without floor-space expansion. One line can switch between, say, a 1.5" B-deck profile for composite concrete floors and a 0.6" form deck for permanent formwork. These two items, together, meet most of the needs of mid-rise building projects in the U.S. It only takes minutes to switch active tools using the PLC instead of hours when you do it by hand.
- Consistent embossing depth across both decks. The 120 mm embossing shaft keeps the shape of the depressions needed for the steel and concrete to mechanically shear together. It is known that composite slabs can fail at shallow embossing. The heavier shaft diameter prevents deflection and keeps depth tolerances tight across the whole coil width.
- Energy distribution across three drive motors. The three 11-kW motors work together to spread out the torque demand, so one big motor doesn't have to work too hard. This stops heat from building up, lowers the immediate current draw, and increases the time between motor service intervals, which is a big plus for lines that work multiple shifts.
Together, these benefits solve the most common problems that deck makers have with production: the time it takes to change profiles, the inconsistent stamping, and the extra energy use. In reality, a double deck roll forming machine line can meet the needs of two different projects from the same operator station during the same shift.
Typical end-use applications include composite concrete floors in high-rise towers, mezzanine decks in logistics warehouses, roof decks beneath insulation and membrane systems, and permanent form decks in parking structures — all product categories experiencing sustained demand across U.S. construction markets.
Double Deck vs. Single Deck Roll Forming Machines: A Comparative Analysis
Matching Machine Type to Production Reality
It comes down to order mix and floor space when deciding between a double deck roll forming machine and a dedicated single-profile machine. A single-deck line costs less up front and has better output for one shape. It works well for manufacturers whose only product is a uniform type of deck that is bought in large quantities under long-term contracts.
A dual-profile line costs more at first, but it pays for itself by cutting down on tooling switching time and making it easier to reply to mixed-profile bids without having to reschedule. When contractors make their own decks, the needs of each job are different, so the price difference in the first contract cycle is often worth it because they can be flexible with timing.
Two separate lines run in parallel in tandem roll forming systems, which have the highest raw throughput but need about twice as much floor space and twice as many operators. They make sense when the annual tonnage is very high, and both profiles run at the same time and all the time. There is a better balance between a single-profile line and a full tandem installation that most mid-scale deck makers find with a double deck roll forming machine.
When to Buy a Double Deck Roll Forming Machine: Decision Support Guide
Four Procurement Scenarios That Justify the Investment
When the decision to invest capital is made is just as important as what the machine is made of. If any of the following apply to your business, you might want to buy a dual-profile steel deck line:
- Your project pipeline includes both composite floor deck and form deck within the same contract year. Running two profile families on one line cuts down on machine downtime between project steps that are specific to each profile.
- Floor space is constrained, but output requirements are growing. The small dual-tooling frame gives you the profile range of two separate lines in the space of one. This math is very important for urban fabrication sites or combined contractor shops.
- You need ASTM-compliant profiles with reliable embossing for composite slab specifications. The CR12 hardened blades and 120 mm embossing shaft are designed to meet the exact size and surface standards set by structural engineers for composite action.
- You are entering new geographic markets or tender categories. The same base machine can meet different regional deck standards without having to buy a second machine. This is possible because OEM tooling modifications can cover rib shapes from 0.6" form deck up to 1.5" A/B rib and up to 3.0" composite and dovetail profiles.
When looking at different suppliers, make sure they have ISO 9001 certification, CE compliance if needed, and documented examples of previous installations in similar construction markets. Check the drive control specs. PLC and converter systems based on Siemens have a large service network across North America, which is important for getting extra parts over time and doing diagnostics from afar.
Conclusion
A double deck roll forming machine solves the main problem that tension deck makers face: they need to make different structural shapes without having to spend more money on equipment or take up more floor space. These machine specs—95 mm forming shafts, 120 mm embossing shafts, CR12 hardened cutters, 3 × 11 kW distributed drive, and 10–20 m/min line speed—are based on engineering decisions that take into account real production stresses rather than theoretical benchmarks. The dual-profile architecture gives a clear return on investment, whether you are expanding a deck-making business, adding production to a steel-building contracting company, or setting up a new fabrication facility.
FAQ
1. What materials can a double deck roll forming machine process?
The machine processes galvanized steel (Z275–Z600 finish) and Galvalume coil with a width of 0.8 mm to 1.2 mm and a minimum yield strength of 235 MPa. These specs describe the coil types that are most often used for structural floor and roof deck in business and industrial buildings in the U.S.
2. How long does a profile changeover take between the two decks?
The operator changes which deck is active through the PLC interface because both sets of tools stay in place in the machine frame. The physical shift time is much faster than a normal retool. Depending on the coil threading needs, it is usually measured in minutes instead of hours.
3. What maintenance does the embossing shaft require?
The part of the forming train that has to handle the most load is the 120 mm embossing shaft. As part of regular maintenance, the shaft bearings are oiled, the knurl depth is checked after long high-gauge runs, and the chrome surface wear on the forming rollers is checked. A good starting point is to have scheduled inspections every 500 hours of operation.
4. Is CE certification relevant for U.S. buyers?
When a double deck roll forming machine has CE certification, it means that it meets the safety and documentation standards set by the EU Machinery Directive. Although it's not required by U.S. law, it shows a confirmed level of technical rigor that protects design, electrical safety, and the completion of paperwork. Many U.S. procurement teams use this as a sign of a supplier's trustworthiness when they're evaluating them.
Get a Custom Quote on Your Steel Deck Line — Contact ZTRFM Today
Roll-making equipment from ZTRFM has been sold to customers in more than 150 countries since 2014. The company is certified by ISO 9001, CE, and CAS. You can change the OEM rib shape, embossing rollers, and inline punching on our double deck roll forming machine that we have for sale. To get a custom quote and specification, email our engineering team at zhongtuorollforming@gmail.com. We can help you whether you need a single machine or a full smart production line.
References
1. Steel Deck Institute. SDI Manual of Construction with Steel Deck. Steel Deck Institute, 2017.
2. American Iron and Steel Institute. Cold-Formed Steel Design Manual. AISI, 2016.
3. Hancock, G. J. Cold-Formed Steel Structures to the AISI Specification. Marcel Dekker, 2001.
4. ASTM International. ASTM A1008/A1008M: Standard Specification for Steel, Sheet, Cold-Rolled, Carbon, Structural. ASTM International, 2022.
5. European Committee for Standardization. EN 10346: Continuously Hot-Dip Coated Steel Flat Products for Cold Forming. CEN, 2015.
6. Pekoz, T., and Schafer, B. W. "Recent Advances in Cold-Formed Steel Structural Members and Systems." Journal of Constructional Steel Research, 2009.