- English
- French
- German
- Portuguese
- Spanish
- Russian
- Japanese
- Korean
- Arabic
- Irish
- Greek
- Turkish
- Italian
- Danish
- Romanian
- Indonesian
- Czech
- Afrikaans
- Swedish
- Polish
- Basque
- Catalan
- Esperanto
- Hindi
- Lao
- Albanian
- Amharic
- Armenian
- Azerbaijani
- Belarusian
- Bengali
- Bosnian
- Bulgarian
- Cebuano
- Chichewa
- Corsican
- Croatian
- Dutch
- Estonian
- Filipino
- Finnish
- Frisian
- Galician
- Georgian
- Gujarati
- Haitian
- Hausa
- Hawaiian
- Hebrew
- Hmong
- Hungarian
- Icelandic
- Igbo
- Javanese
- Kannada
- Kazakh
- Khmer
- Kurdish
- Kyrgyz
- Latin
- Latvian
- Lithuanian
- Luxembou..
- Macedonian
- Malagasy
- Malay
- Malayalam
- Maltese
- Maori
- Marathi
- Mongolian
- Burmese
- Nepali
- Norwegian
- Pashto
- Persian
- Punjabi
- Serbian
- Sesotho
- Sinhala
- Slovak
- Slovenian
- Somali
- Samoan
- Scots Gaelic
- Shona
- Sindhi
- Sundanese
- Swahili
- Tajik
- Tamil
- Telugu
- Thai
- Ukrainian
- Urdu
- Uzbek
- Vietnamese
- Welsh
- Xhosa
- Yiddish
- Yoruba
- Zulu
Roll Former Keeps Stopping: 7 Trips to Check First
When a PLC controlled roll forming machine keeps stopping, check seven areas first: the emergency stop and safety circuit, motor and inverter protection, sensors and encoders, hydraulic or pneumatic pressure, material alignment, cutting synchronization, and power or heat conditions. The PLC usually reports a symptom, not the root cause. A loose limit switch or a dirty sensor can send the same fault again and again, no matter how often you reset. I recommend working through these checks in order and recording what you find. That habit usually locates the problem faster than swapping parts.
First Response: Before You Reset the Machine Know Which Kind of Stop You Have
When you look at the HMI, a safety stop, a process slowdown, a mechanical jam, and an electrical problem may all look the same. However, they need to be fixed in different ways. If you push a button or open a guard, the machine will stop safely. The process stops while the PLC looks for a signal, like the home point of the cylinder. When something blocks the wheels, you have a jam. There are many signs that something is wrong with the power, such as a drive code, a tripped breaker, or lost contact. Before you pick up a tool, putting the stops together can help you narrow down your search.
Record the Details Before You Reset
The HMI message, the warning code, the line speed, the material of the coil, the profile, and the stage of the stop should all be written down. For example, write down when it was first turned on, when it was being made, when it was being cut, or after a long run. Most of the time, a fault that shows up after an hour is caused by the heat. Most of the time, the cutting unit is to blame when a fault shows up after every cut. Before you open the cabinet or go into a dangerous area, you need to lock out and tag out the power. OSHA standard 29 CFR 1910.147 talks about controlling energy while in business. It is never a good idea to go around emergency stops, guards, hydraulic interlocks, or other safety features.
Why Repeated Resets Cost More
Every time, it gets the same amount of stress. All three are broken when the engine starts up at full speed and the drive trips because of too much load. Cutting tools can be bent if a profile gets stuck, and the blade can only be turned halfway if the pressure signal is weak. It gets rid of hints too. First, look at the alarm data and see if it matches what you see on the machine when it comes to the input and output states. After that, read the code for the drive fault. The PLC helps you the most when it tells you what it was waiting for.
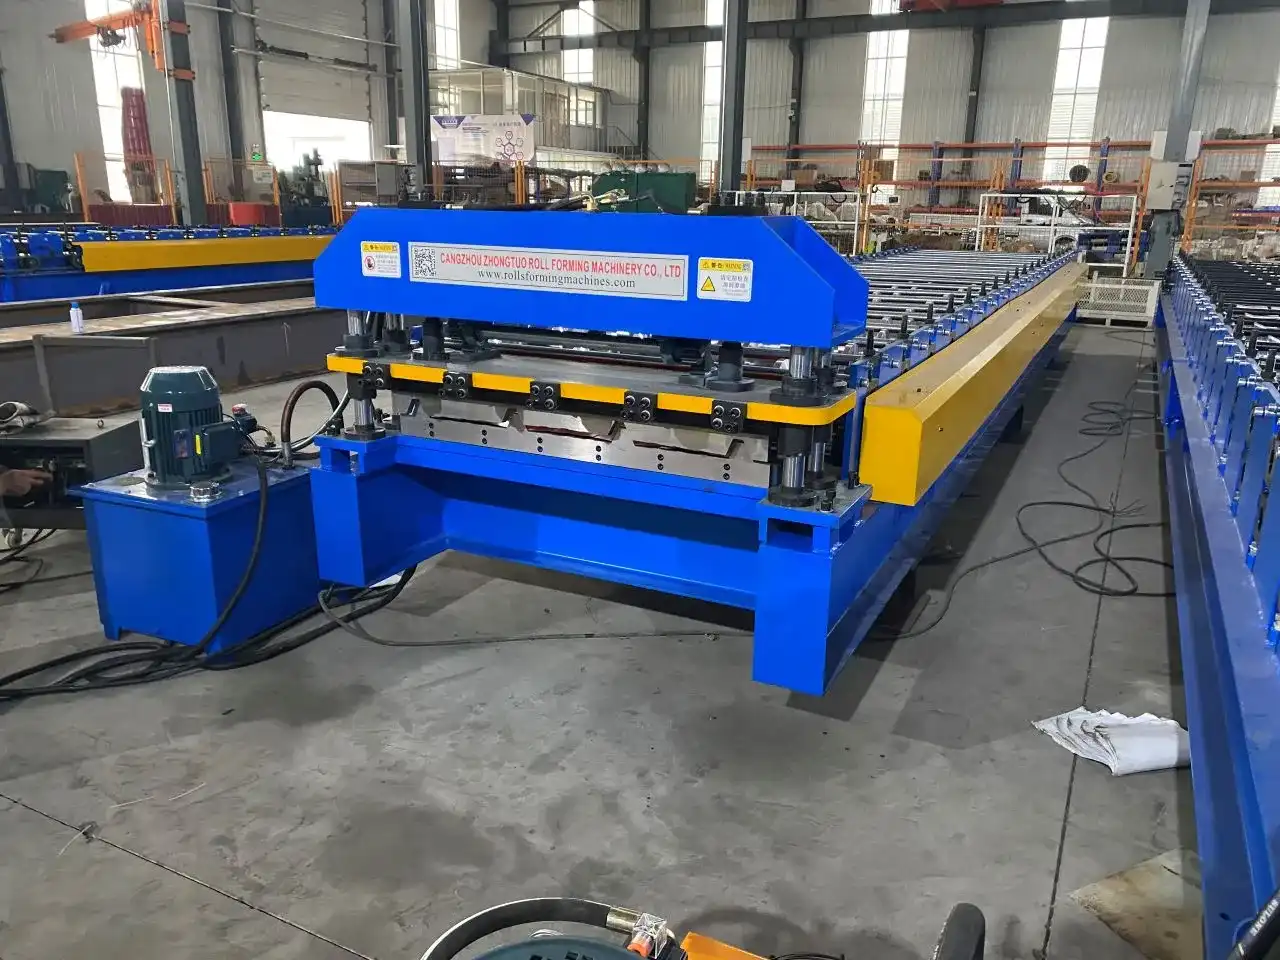
Trips 1–4: Safety, Drive, Sensors, and Fluid Power
Trip 1: Emergency-Stop or Safety Circuit
A safety trip could stop the whole line, even if nothing is broken. It is important to check every guard switch, emergency stop button, remote station, and safety relay, even the ones that are close to the cutting unit and run-out table. Voids can damage lines, make connections loose, or move a switch out of place, all of which can cause false trips. If there is a safety delay, the signal that turns on the drive can be turned off. But other parts of the electricity would still work, so the picture would still look good. Once the trigger has been found, it should not be reset. After that, test it at a slow speed with all the safety features on.
Trip 2: Motor, Inverter, or Overload Protection
If the temperature, current, power, or voltage gets too high, the drive may shut down. Check the screen to see if it shows any transmission codes, overcurrent, overload, overvoltage, undervoltage, smoke, or overcurrent. It's often the first sign that something is wrong with the power when a motor does not work right. If there is too much pressure, poor cleaning, the wrong material going in, or damage to the shaft, the motor load can go up. As the sheet's speed, thickness, and acceleration change, you can see how the fault time changes too. The problem should be checked if it goes away when the speed is slowed down. The shape, cut, and put process is set up by the PLC with the help of sensors and encoders. See if it stays by checking the motor and drive during PLC control failure troubleshooting.
Trip 3: Sensor, Encoder, or Input Failure
If the limit switch is moved, the connector is loose, or the cable is broken, the line could stop while the screen shows a process fault. If you want to make sure the encoder works, make sure the wire is secure, and make sure the unit can spin freely. Check the length of the piece you're done with against the length shown. If they don't match, there may be a problem with the feedback. For that reason, keep signal wires away from power hookups. Close drives and electrical noise can also mess up signals.
Trip 4: Hydraulic or Pneumatic Pressure Loss
A lot of fluid power is used for cutting, locking, cut-off units, and tool return. The next PLC step can't happen because there isn't enough air, a leak, a clogged filter, hot oil, or a worn-out cylinder. If you only look at the pressure gauge when the machine is not in use, everything might be fine. Maybe the PLC is waiting for a signal from a button that you press hard or from the "home" setting. Check both the part and the pin that goes into it. Before you go back to full speed, fix any leaks or air that isn't tight.
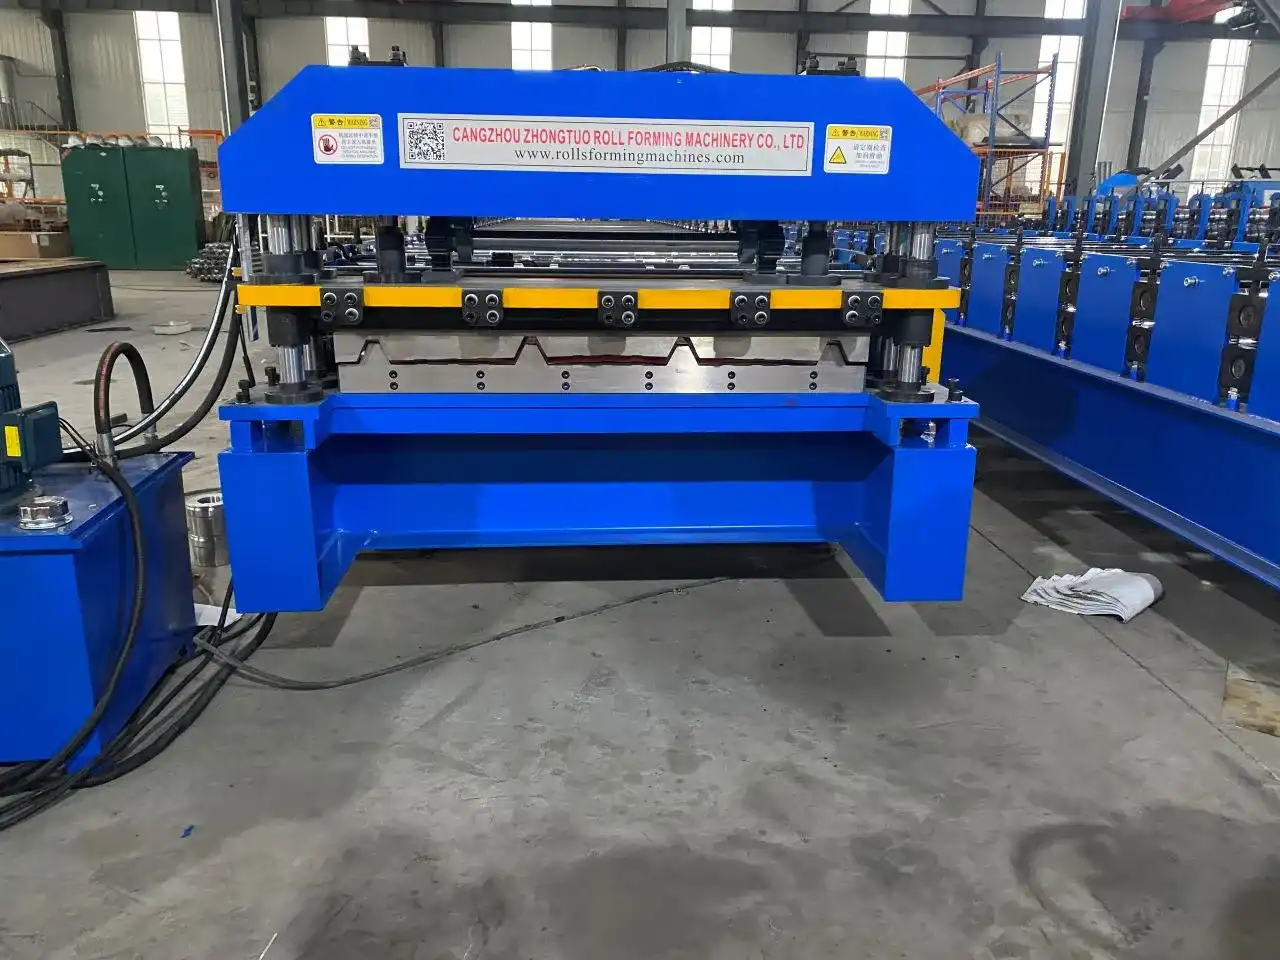
Trips 5–7: Material, Cutting, and Electrical Conditions
Trip 5: Material Misalignment and Roller Problems
As a general rule, problems are caused by material that doesn't fit the way the machine was built. The width, thickness, yield strength, edge burrs, telescoping, and uncoiling tension of the coil are all things you should think about. The strip can be pushed off-center, though, and the forming resistance can rise if the entry guides, leveler rollers, or forming stations are not set up correctly. It's possible for the drive to fill up. Check out the shaft, the bearings, the bolts, and how far apart the rollers are. Also, look at the profile to see if there are any twists, waves, scratches, or buildup. Next, run a coil that is the right size and has clear lines that show where the flaws are in the material and where they are in the machine.
Trip 6: Cutting System and Length Synchronization
The moving shape, the encoder input, and the cut-off length should all be the same. If a blade, punch, die, or cylinder doesn't fully return, the next run can be stopped. Check the home-position sensors, the hydraulic pressure, the movement of the cylinder, and any scrap metal that is close to the cutter. Record the length that was programmed and then compare it to the length that was programmed. It's very important to do this if the encoder coupler can move. Not being in line can also happen if the setting is too fast, too slow, or too short. In this case, a custom PLC-controlled roll forming machine might need different cutting recipes for each material, shape, and thickness.
Trip 7: Power, Wiring, Communication, and Heat
The electricity sometimes goes out, but only after long runs or after the cabinet has warmed up. It is important to check the tightness of the terminals, the phase balance, the voltage stability, the control voltage, and the breakers and transformers during PLC control failure troubleshooting. These are the Ethernet or fieldbus wires that connect the PLC, HMI, inverter, motor drives, and remote I/O. Make sure there are no breaks in them. Clean the fans, screens, and vents in your closet. People often put the blame on the PLC when they shouldn't because dust, water, rust, and heat can make the drive stop and start randomly and cause problems with no technical sign.
From Troubleshooting to Prevention and Purchasing
Diagnose Systematically and Keep Records
It takes a while to change parts that were put together incorrectly. Take note of all the alarms that go off, make sure the power and safety are on, check the PLC's inputs and outputs, and make sure the fluid or mechanical system that is linked is working right. Plan when the test should end. Last, run the tests slowly and without any load. In a log, you can write down your material, profile, speed, temperature, warning code, fix, and test result. To back up the PLC and HMI settings, do what the maker tells you to do. Sensors, leaks, guards, rollers, noise, and heat can all be found early on if you check them every day.
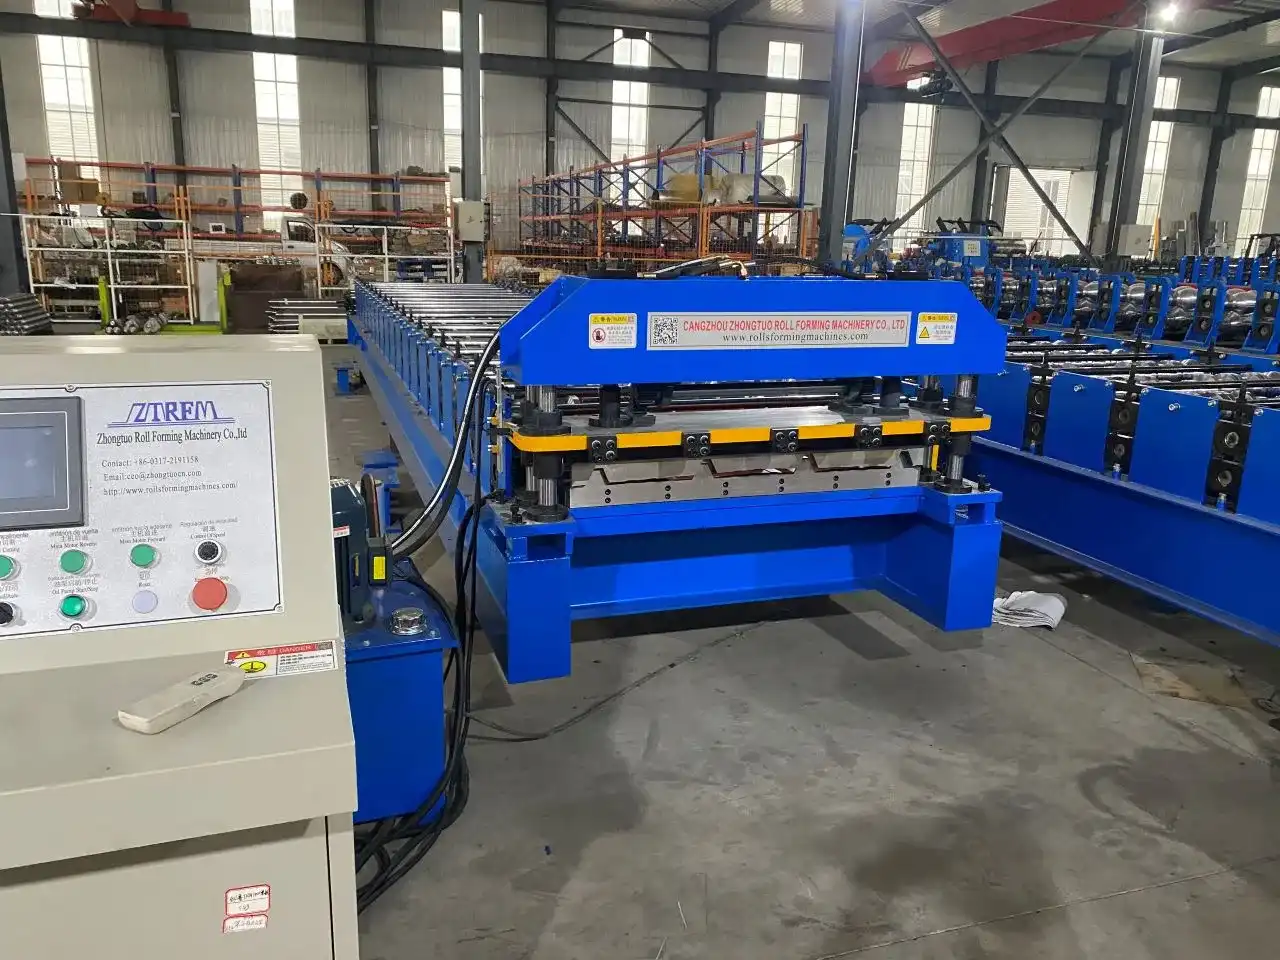
Repair, Retrofit, or Replace
For stops that happen over and over, you don't need a new PLC. It makes sense to fix the processor if the problem is with the wiring, sensors, drives, parameters, or mechanical parts. When the PLC or HMI is out of date, the symptoms are bad, contact is lost a lot, or parts are hard to find, retrofitting is a good option. It's possible that some parts of the machine are old, or it might not be fast enough, accurate enough, able to cut well enough, or automated enough for your needs. Maybe getting a new line will save you money in the long run. You should think about things like downtime, the cost of upgrades, lost work, the help that's available, and what the future might hold.
Choosing a PLC Controlled Roll Forming Machine
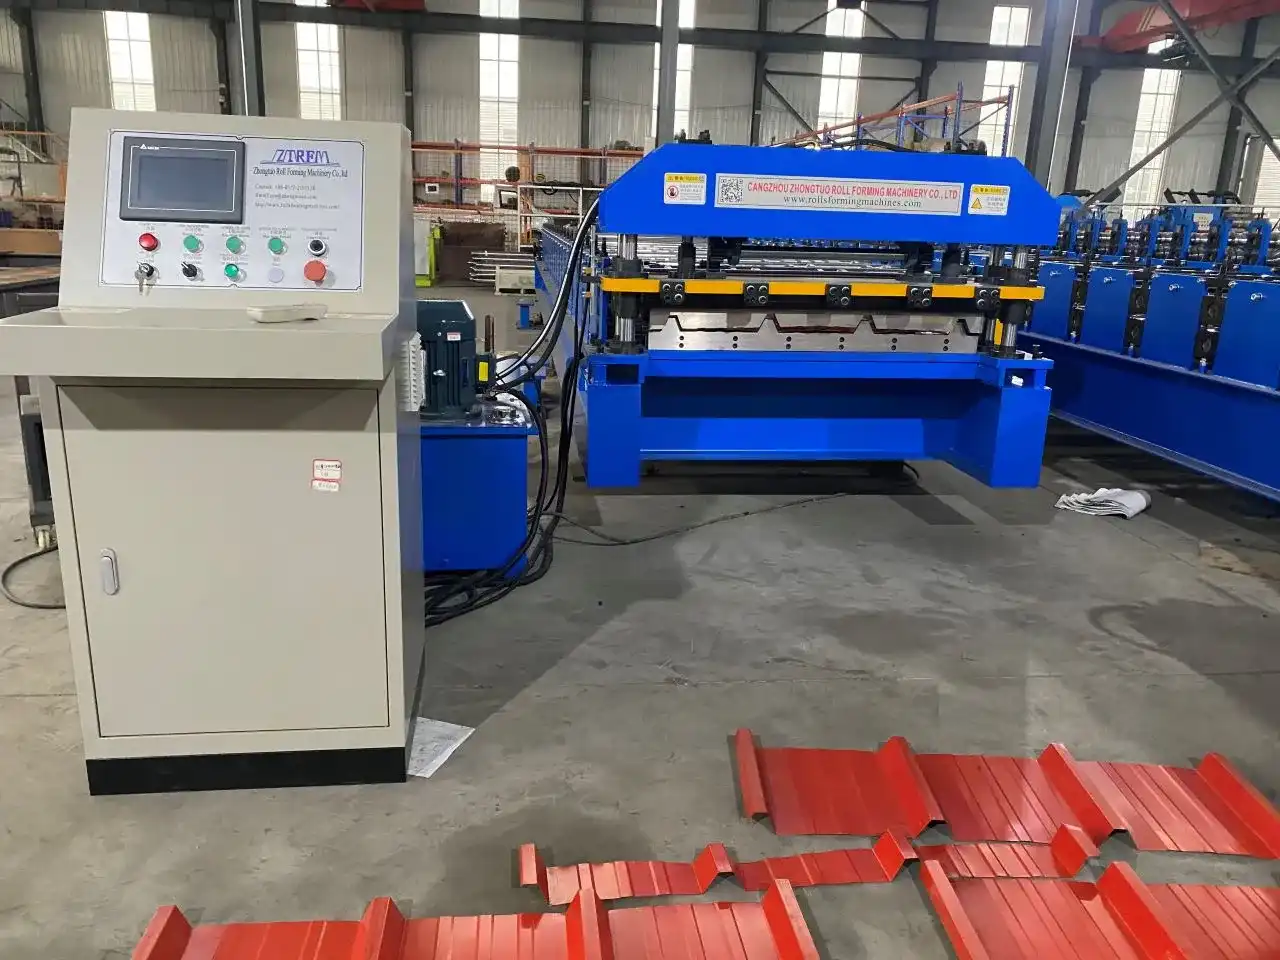
Don't just look at the cost and speed. Ask the seller what kinds of PLC-controlled roll forming machine brands they sell, including HMI, inverters, and servos. Find out if the machine has a history of alarms, a place to store recipes, a way to back up data, a way to fix from afar, and wiring drawings. Make sure the specs match the type of material, its thickness, width, profile, output goal, and the difference in cut length. Rolling lines are made by ZTRFM for roofing sheets, C purlins, ridge caps, and standing seam panels, among other things. A PLC runs these lines, and hydraulics are used to cut them. Send a short film, the model, the serial number, photos of the warning, the drive codes, and profile drawings when you ask for help or a price.
Conclusion
If a PLC controlled roll forming machine stops working a lot of the time, it's probably not the PLC itself that's broken. Some of the things that can cause a warning are the drive protection, the fluid pressure, the material alignment, the cutting timing, and the power or heat conditions. The procedure stays the same if the warning, stopping point, and working conditions are written down before the device is restarted. The history of alarms and the I/O status help figure out what's wrong, and a physical check proves it. It's better to check, log, and back up settings on a regular basis so that things don't stop all of a sudden. You should decide whether to fix, retrofit, or replace based on how much downtime you have, how much production you need, and how much support you need for parts.
FAQ
1. Why does my machine stop with no clear alarm?
A lot of the time, vague warnings are caused by unstable inputs, loose wires, lost contacts, power drops, or the box getting too hot. The safety can also be set off by the machine being overloaded. Before you do anything else, check the plugs, the weather, and the power source.
2. How often should I inspect the machine?
Every day, check the guards, sensors, rollers, sounds, heat, and leaks. Depending on how they are used and what the manufacturer says, you should lubricate, clean, and take care of the filters, encoder couplings, and terminals once a week or once a month.
3. Should I replace the PLC first?
Not at all. Most of the time, the machine stops when something goes wrong with the lines, sensors, drives, hydraulics, or materials. First, you should see if the controller is broken.
4. What should I ask a supplier?
Find out about the length accuracy, the part brands, the electrical documentation, the warranty terms, spare parts, and how it will be used.
Get Technical Support from ZTRFM for Your PLC Controlled Roll Forming Machine
Why do you need to stop? ZTRFM can check into it or give you a new line price. To zhongtuorollforming@gmail.com, you can send pictures of the alarm, model details, material data, and profile drawings. When looking for a PLC controlled roll forming machine manufacturer, you should be clear about who you are, the materials you want to use, how much you want to produce, how much of a range you are willing to accept for cut lengths, and how much automation you need. Our techs can train you, test, set up, and help you get new parts. They can give you either a standard or a unique answer.
References
1. NFPA 79: Electrical Standard for Industrial Machinery, 2024
2. OSHA 3120: Control of Hazardous Energy (Lockout/Tagout), 2002
3. ISO 13850: Safety of Machinery – Emergency Stop Function, 2015
4. IEC 61131-3: Programmable Controllers – Programming Languages, 2013
5. Programmable Logic Controllers (Frank Petruzella, McGraw-Hill), 2016
6. Machinery's Handbook, 31st Edition (Industrial Press), 2020