- انګلیسي
- د فرانسې د
- د آلمان د
- پرتګالي
- اسپانوی
- روسی
- د جاپان د
- کوریایي
- عربي
- ائيرلېنډي
- یوناني
- ترکي
- ایټالوی
- ډنمارکي
- رومانیایی
- اندونېزیايي
- د چک
- د کلکسینونو له
- د سویډن د
- صیقل
- باسک
- کتلان
- یا بروز کول
- هندي
- لاو
- کلمات په
- اماري
- د ارمنستان
- د اذربایجان د
- بلاروسي
- بنګالي
- د بوسنیا
- د بلغاریا
- cebuano
- Chichewa
- کورسیکن
- کرواسین
- هالینډي
- استونیا
- فلیپیني د
- فنلڼډي
- فريزي
- ګلېشيايي
- د ګرجستان
- ګجراتي
- هایتین
- هوسا
- د هاوایی
- عبراني
- همونګ
- هنګري
- ایلینډیک
- igbo
- جاوايې
- کناډا
- د قزاقستان
- خمېر
- کردي
- د قرغزستان
- لاتیني
- لېټواني
- لیتوانیایي
- لوګزامبو..
- مخدوني
- Malagasy
- مالیزیایي
- مالايلام
- مالټایي
- ماوري
- مراټي
- منګولیایی
- برمایی
- نېپالي
- ناروې
- پښتو
- فارسي
- د پنجابي
- سربي
- سيسوتو
- Sinhala
- سلواک
- سلوانیایي
- د سومالیا د
- سموني
- سکاټلېنډي ګېلک
- شونا
- سندي
- سوډاني
- سواهیلي
- تاجک
- تامیل
- یا بروز کول
- تایلېندي
- د اوکراین
- اردو
- ازبک
- ویتنامي
- ګوجراتي
- خوسا
- عبراني
- یوروبا
- Zulu
کوم رول فارمر د سولر کارپورټ بریکٹ تولید لپاره مناسب دی؟
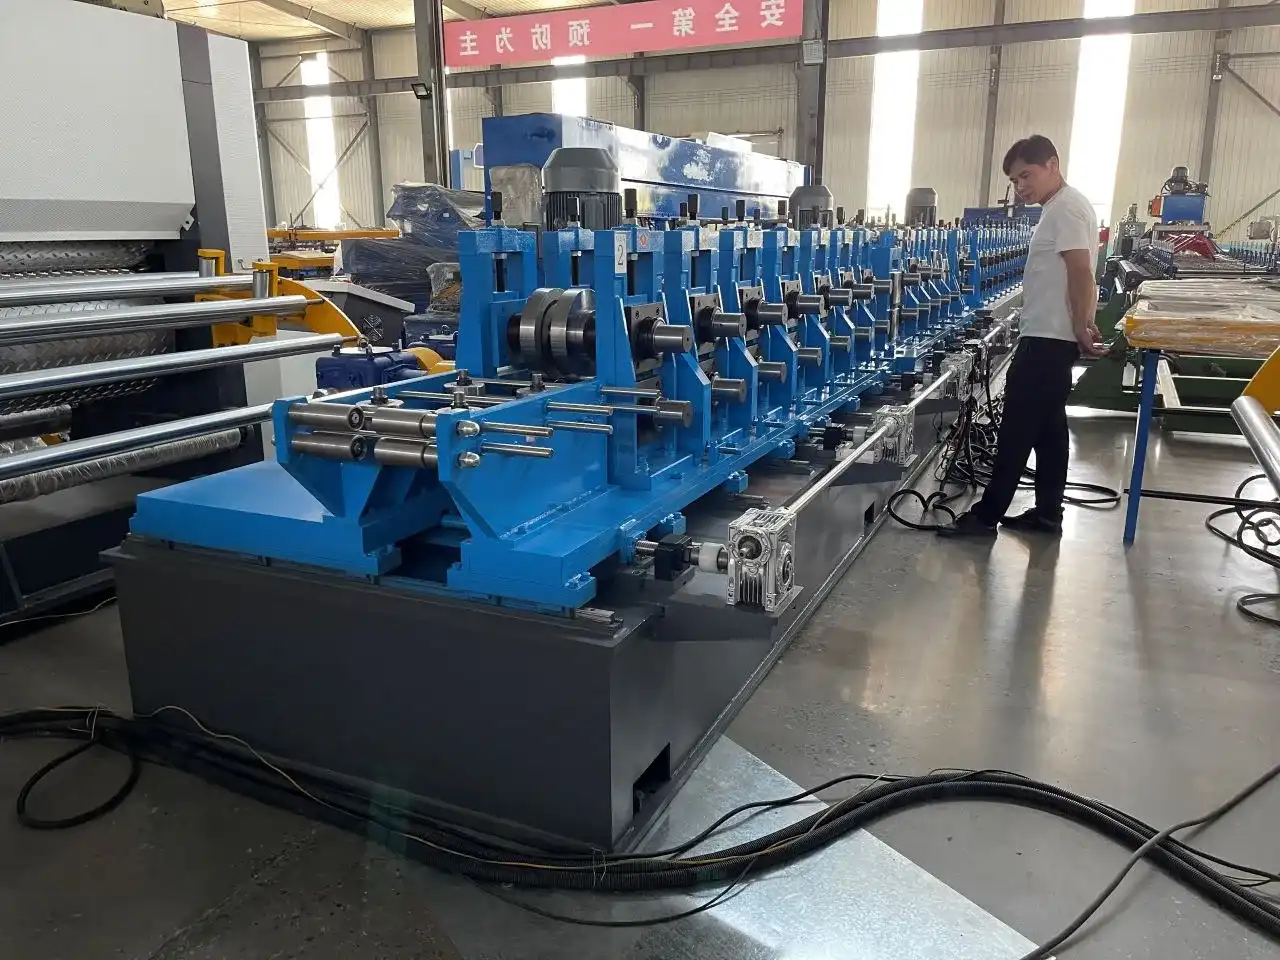
A د سولر سټرټ چینل رول جوړولو ماشین with inline punching is best for solar carport bracket production. Carport frames need accurate C-channel and strut profiles with slot holes in the right places. I recommend matching the machine to your profile drawing, steel thickness, and monthly output before you compare prices. The ZTRFM line forms 1.5–2.5 mm coil, accepts a feeding width of 90–230 mm, and runs at 8 m/min with hydraulic shearing. It also offers online, press, or offline punching. Below, I explain how to define your needs, compare configurations, check specifications, and judge suppliers.
Why Solar Carport Bracket Production Needs the Right Roll Former Profile Accuracy Shapes Assembly and Load Transfer
As a result of the fact that solar carports are used to support photovoltaic modules above parking spots, each strut, C channel, and rail must be able to securely handle wind and snow loads. These kinds of constructions are subject to the minimum design loads that are established by ASCE 7, and the design of cold-formed steel members is covered by AISI S100. On site, a profile that has a flange angle that is incorrect or a hole that is not properly positioned will not bolt up neatly. Following this, crews either drill new holes or push items into position, both of which slow down the installation process. Cut length is also important since even little mistakes might add up over the course of a lengthy beam row.
Common Production Problems
The majority of roll forming operations are confronted with the same four challenges: material deformation, uneven dimensions, sluggish changeovers, and excessive scrap. When the forming stations are unable to bend the strip progressively during the process, deformation manifests itself as bow, twist, or flared ends. Inconsistent dimensions are often the result of tooling that is loose or shafts that are weak. When you run various lengths or hole patterns for each one of your carport designs, slow changeovers reduce the amount of output you get. Due to the fact that each handling stage adds an additional mistake, scrap increases when punching and cutting are performed in separate processes. Many of these issues may be eliminated by a single continuous line.
Why a General C Channel Machine Falls Short
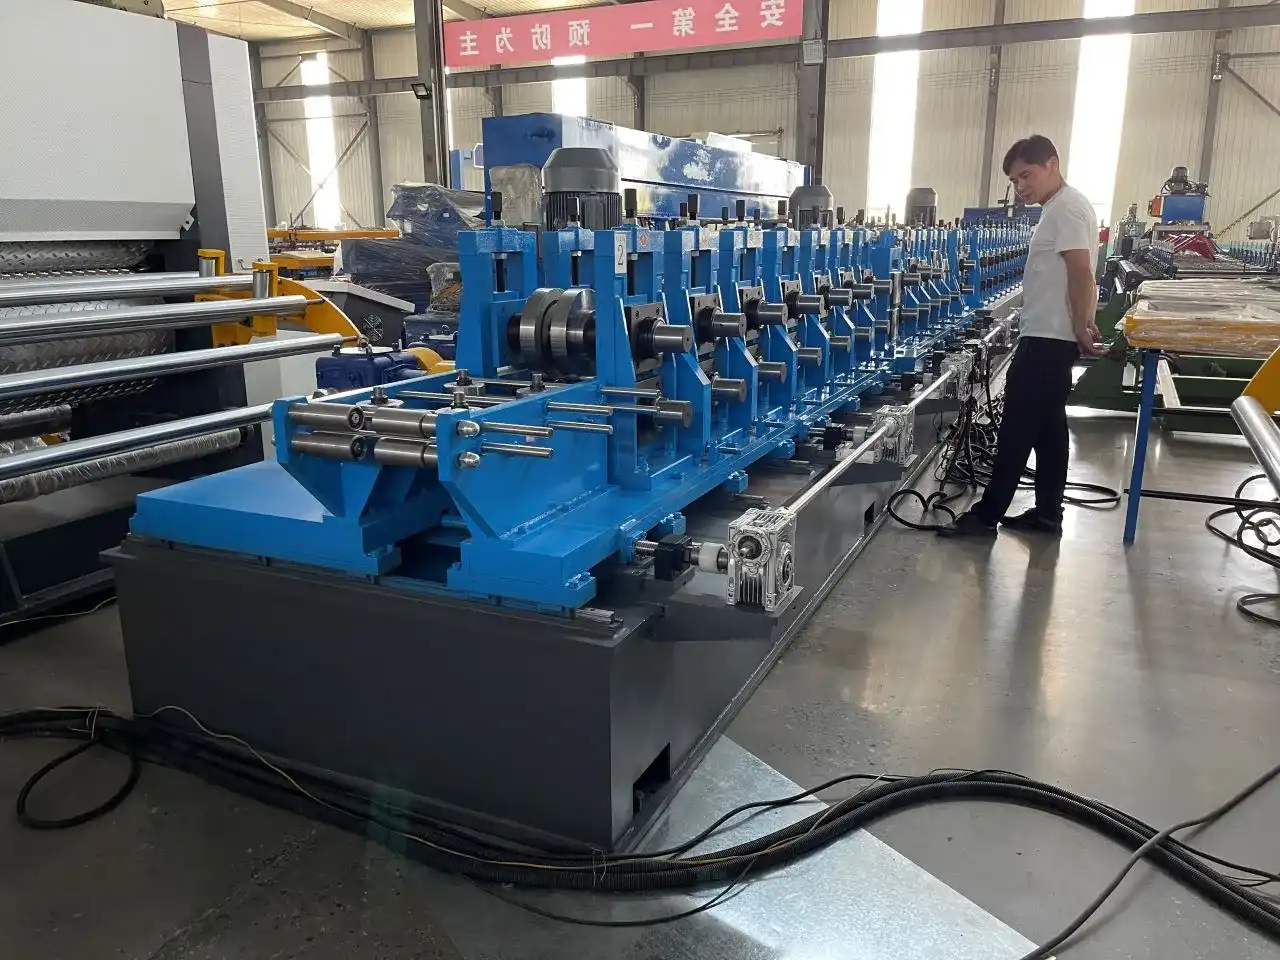
A general-purpose C channel roll forming machine can make a plain section, but solar profiles ask for more. Strut channels need slot holes at set pitches, a clean cut, and lips that stay square after punching. Without inline punching, you need a second press and extra handling. Without customized roll tooling, each new carport design means a long wait or a compromised profile. A dedicated د سولر سټرټ چینل رول جوړولو ماشین joins leveling, punching, forming, cutting, and stacking, so hole position and profile stay linked from the first meter to the last.
Define Your Requirements and Pick the Right Configuration
Start With Profile, Material, and Output
It is important to make a note of the profile type before requesting a price. This might be strut, C, U, slotted, or rail. After that, make a list of the steel grade, coating, thickness, coil width, hole geometry, pitch, cut length, and number of tonnes produced each month. Drive shaft size, motor power, and the number of forming stations are all factors that are determined by thickness and yield strength. When it comes to material, the ZTRFM line handles 1.5–2.5 mm. Let us know as soon as possible if the design of your carport requires steel that is either thicker or of a greater strength so that our engineers can change the tooling and drive. A thorough brief eliminates the need for revisions and ensures that quotations are comparable.
Separate Rated Speed From Real Capacity
It is not possible for a line that is rated at 8 meters per minute to operate at that speed during the whole day. Alterations to the coils, setup, punching, cutting, maintenance, and operator inspections are all activities that need time. One hour of continuous running at maximum pace results in 480 meters; however, the actual distance you cover is contingent on the hole design, the length of the cut, and the number of hours you run. Request that each provider provide a capacity estimate based on your personal profile rather than a standard sample. The line may be sized to accommodate your orders rather than a brochure with the aid of this number.
Dedicated, Semi-Automatic, or Multi-Profile
When it comes to big volume, a dedicated automated line is suitable for one steady profile. Although it requires more labour, a semi-automatic line is more cost-effective and can accommodate smaller quantities. Manufacturers and distributors that supply many carport designs are ideal candidates for a multi-profile line. Through the use of fast roll change or servo adjustment, ZTRFM machines have the capability to manufacture sizes such as 41×41, 41×21, and 41×62. There are three different types of punching: online punching, which is used for bulk manufacturing; press punching, which is used for intricate hole patterns; and offline punching, which is used for customised or small quantities. The volume, profile range, and growth strategy are the factors to consider.
How a Solar Strut Channel Roll Forming Machine Works and What to Compare
The Process From Coil to Stack
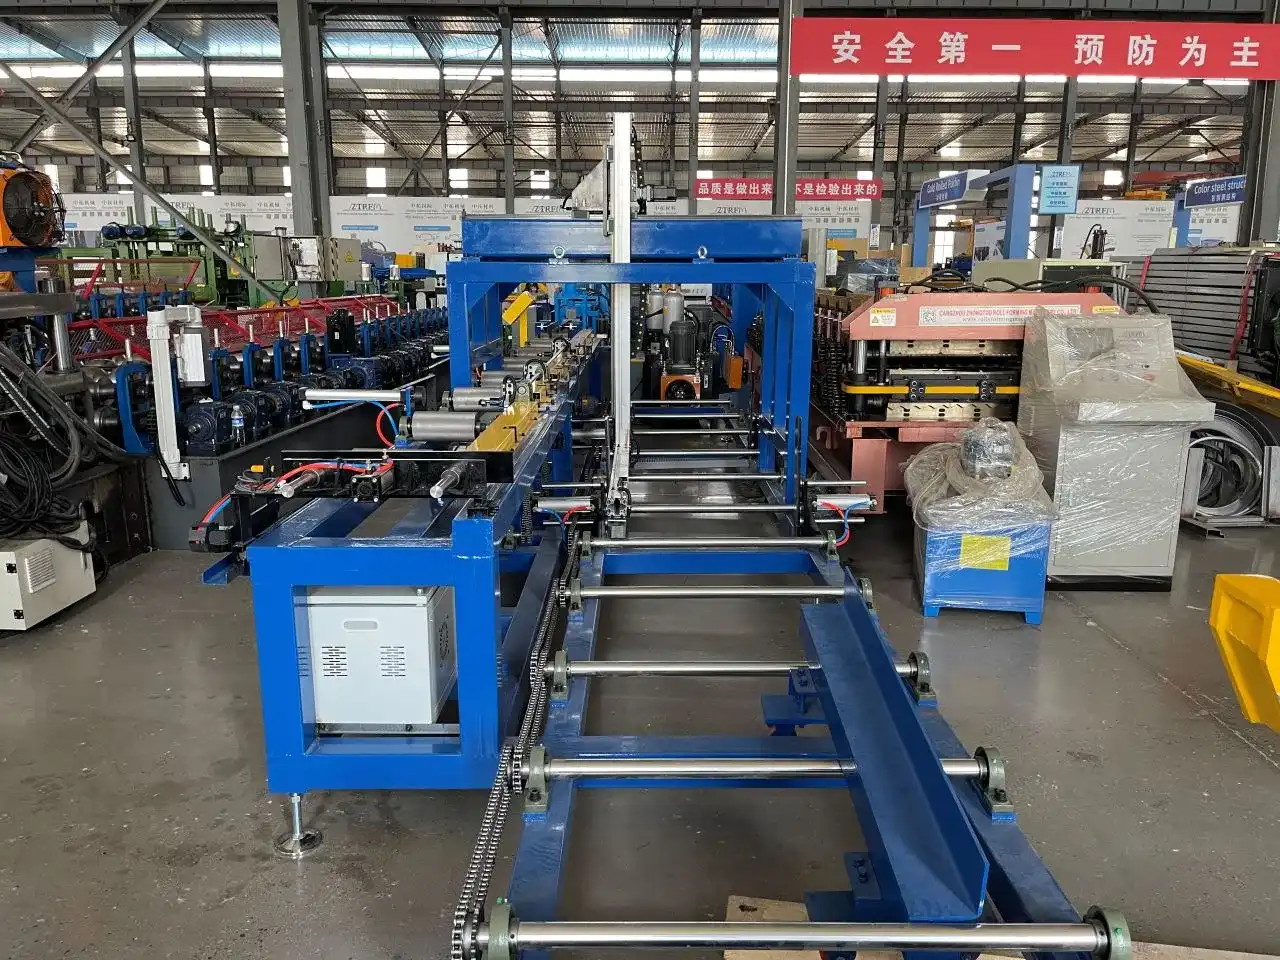
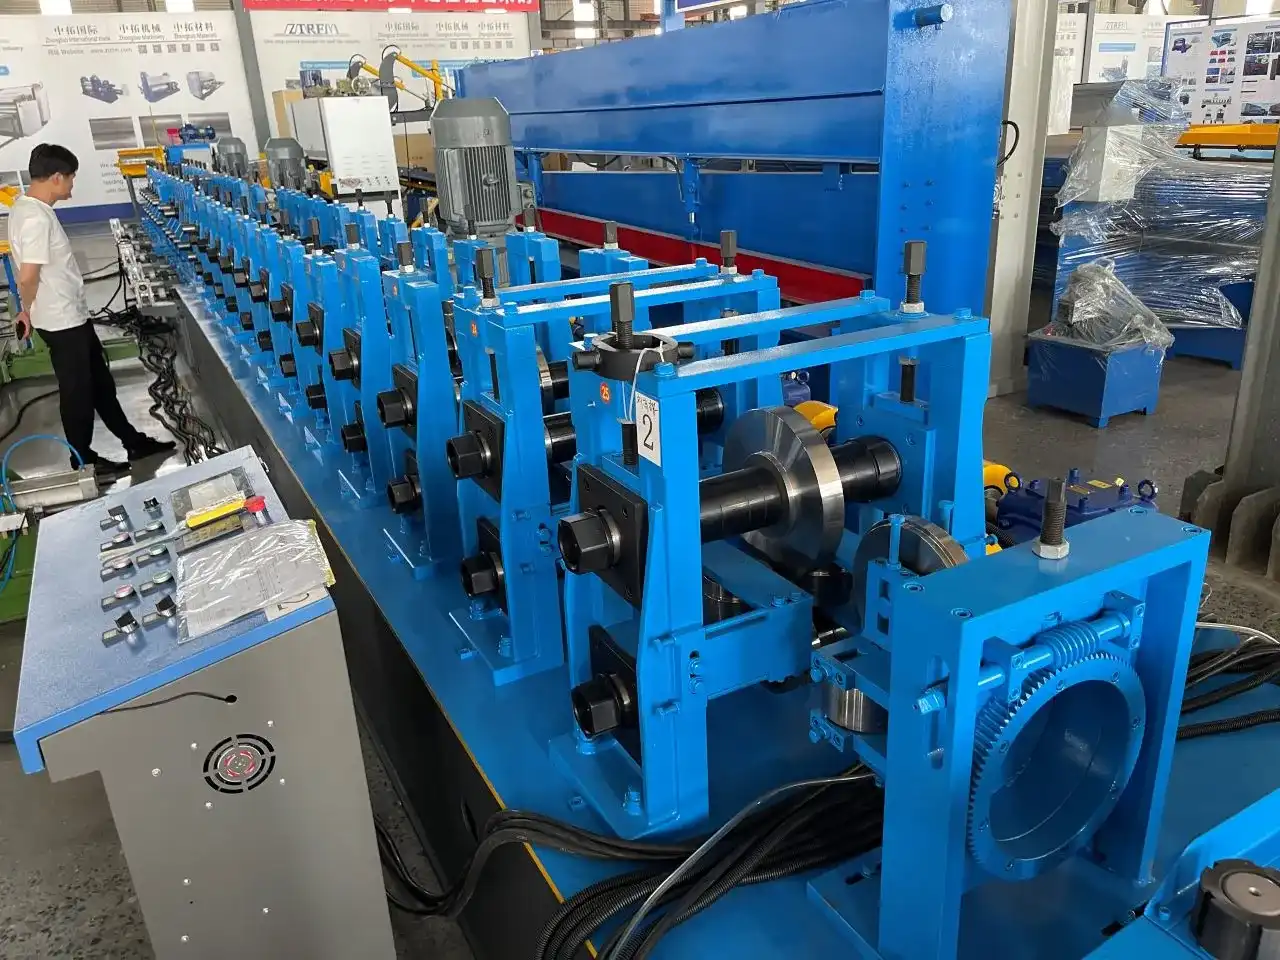
There is just one route that the line takes, which is as follows: coil, levelling, punching, roll shaping, cutting, and stacking. There is a ډیکویلر that retains the coil, and there is a leveller that removes the coil set so that the strip may enter flat. Following the formation of the flat strip, the punching unit creates slot holes in the strip. The steel is then bent by 24 rollers in a step-by-step manner, which prevents the strip from unexpected stress. The length of each piece is determined by hydraulic shearing, and the completed channels are collected by a run-out table and a stacker thereafter. Triggering the length, counting, and triggering alerts are all coordinated by the PLC control.
د چک کولو لپاره مشخصات
د solar carport bracket production, compare every supplier against the same technical specifications. The ZTRFM line features a 22 kW main motor, an 11 kW hydraulic station, 24 rollers, and an 80 mm shaft made from 45# forged steel. The machine body uses 25 mm 45# steel, while a double-chain drive operates the forming stations. Forming rollers are made from chrome-coated GCr15 steel, and cutter blades use Cr12 mold steel, quenched to 58–62 HRC. The stated tolerance is ±1.5 mm. Compare these specifications with your approved profile requirements rather than evaluating motor power or production speed alone.
Controls and Electrical Compliance
The controls have the same impact on daily production as the steel and shafts do. PLC control with a touchscreen is used for ZTRFM lines, and Siemens or Mitsubishi PLCs are among the available possibilities. You should look for automated length setting, counting, and alerts, and if you operate many profiles, you should enquire about the possibility of storing recipes. While you are comparing different vendors, you should also make sure to examine safety interlocks and coil-end detection. It is possible to request additional forms of electricity in addition to our usual voltage of 380V, three-phase, and 50Hz. Please disclose the voltage and frequency of your location at the beginning. The standard supply in the United States is 60 Hz.
Compare Value, Price, and Suppliers Before You Decide
Look Past the Lowest Price
Although the initial price may be modest, the monthly payments may be greater. A less expensive machine that has weak shafts, does not have inline punching, or has delayed changeovers can result in more scrap and labour. When it comes to production, labour, accuracy, flexibility, and maintenance, compare and contrast automated and semi-automatic lines, pre-punching and post-punching, and single-profile and multi-profile systems. The final price is determined by the intricacy of the profile, the strength of the steel, the kind of punching and cutting, the automation, the number of tools, stacking, installation, and the requirements for export. Send the identical brief to each and every supplier, and request an itemised estimate that includes the cost of equipment, tooling, spares, training, shipping, and taxes that are applicable.
Evaluate the Supplier and Test Before Shipment
A reliable provider will conduct testing on your actual stuff and profile. Be sure to enquire about sample runs, the design of tools, installation, training, warranty, replacement parts, and Incoterms policies. In addition to exporting to more than 150 countries, Cangzhou Zhongtuo, which was established in 2014, is certified to the ISO 9001, CE, and CAS standards. AutoCAD, SolidWorks, and COPRA are the tools that our engineers use to build product profiles. It is important to do a thorough inspection of the profile dimensions, straightness, twist, hole size, slot location, pitch, cut length, and burrs with punching and cutting runs before delivery. Manuals, electrical diagrams, and tooling drawings should be requested throughout the handover process.
Custom Solutions and Mistakes to Avoid
Equipment that is standard fits within a single stable profile. Several carport profiles, customised slot designs, stringent tolerances, or OEM tooling are all examples of situations in which customisation makes perfect sense. Mistakes that are often made in the purchasing process include putting faith in theoretical speed, providing designs that are incomplete, neglecting coil restrictions, underestimating changeover time, and skipping after-sales terms. Make sure that the authorised drawings, the steel grade and thickness, the hole pattern, the cut length, the tolerance, the power supply, and the guarantee are all confirmed before you place your order. A dedicated automated line can accommodate a large number of orders, a semi-automatic line can accommodate small batches, and a specialised multi-profile line can accommodate a wide range of requests.
پایله
سم د سولر سټرټ چینل رول جوړولو ماشین for solar carport brackets should match your profile, steel specifications, and output requirements rather than simply offering the highest advertised speed. Accurate profiles and properly positioned slot holes help speed up on-site assembly. Inline punching and gradual forming reduce deformation and scrap, which a general C-channel machine may not achieve as effectively. Defining material thickness, hole patterns, cut length, and actual production capacity allows a fair comparison of dedicated, semi-automatic, and multi-profile options. Shaft size, roller material, frame, drive, tolerances, and controls should be checked against your drawings. Long-term value comes from reducing scrap, labor, and downtime, while suppliers that test your materials and establish clear acceptance criteria help minimize purchasing risks.
FAQs
1. What is a solar strut channel roll forming machine?
It turns steel coil into strut or C channels for PV mounting. Leveling, punching, forming, cutting, and stacking run in one continuous line.
2. Can one machine make several sizes?
Yes. ZTRFM machines can produce sizes such as 41×41, 41×21, and 41×62 through quick roll change or servo adjustment, depending on the design.
۲. د پنچ کولو کوم انتخاب باید غوره کړم؟
Online punching suits mass production, press punching suits complex hole patterns, and offline punching suits small or custom batches.
۵. د نرخ ورکولو لپاره کومو معلوماتو ته اړتیا لرئ؟
Send profile drawings, steel grade and thickness, hole pattern, cut length, target output, plant voltage, and destination.
Request a Solar Strut Channel Roll Forming Machine Recommendation
ZTRFM یو دی د سولر سټرټ چینل رول جوړولو ماشین manufacturer with ISO 9001, CE, and CAS سندونه and customers in over 150 countries. Send your profile drawing, steel data, hole pattern, target output, and plant power to zhongtuorollforming@gmail.com ته زنګ ووهئ. Our engineers will suggest a suitable line, arrange sample testing, and prepare an itemized quote.