- English
- francès
- Alemany
- portuguès
- Castellà
- rus
- japonès
- coreà
- àrab
- irlandès
- grec
- turc
- Italià
- danès
- romanès
- indonesi
- txec
- africaans
- suec
- polonès
- basc
- Català
- esperanto
- hindi
- Lao
- albanès
- amhàric
- armeni
- Azerbaidjan
- bielorús
- bengalí
- bosnià
- búlgar
- cebuano
- chichewa
- cors
- croat
- Holandès
- Estònia
- filipina
- finlandès
- frisio
- gallec
- georgià
- gujarati
- Haitià
- haussa
- hawaià
- hebreu
- Hmong
- hongarès
- islandès
- igbo
- javanès
- kannada
- kazakh
- Khmer
- Kurd
- Kyrgyz
- llatí
- letó
- lituà
- Luxembú..
- macedoni
- madagascar
- malai
- malaialam
- maltès
- maorí
- marathi
- mongol
- Birmà
- nepalès
- noruec
- Paixto
- persa
- punjabi
- serbi
- sesotho
- singalès
- eslovac
- eslovè
- somali
- samoano
- Gaèlic escocès
- Shona
- sindhi
- Sudanès
- swahili
- Tadjik
- tamil
- telugu
- tailandès
- ucraïnès
- urdu
- uzbek
- Vietnamita
- gal·lès
- xhosa
- jiddisch
- Ioruba
- zulú
Roll Forming vs Hydraulic Press: Which Wins on Cost?
When budgetary selections determine your whole manufacturing line, the proper way to fabricate a metal frame is more important than most consumers realize. For every factory owner or procurement manager considering a màquina de marc de porta, the issue isn’t just which technology is “better” – it’s which one will provide you the lowest overall cost for your unique production volume, profile complexity, and long-term objectives. This article exposes the facts about roll forming and hydraulic press technology so you can make an educated, confident purchase.
Understanding Roll Forming and Hydraulic Press Technologies
Before you look at prices, it's helpful to know how each system works and where it fits best in the process of making door frames.
Com funciona el perfilat enrotllat
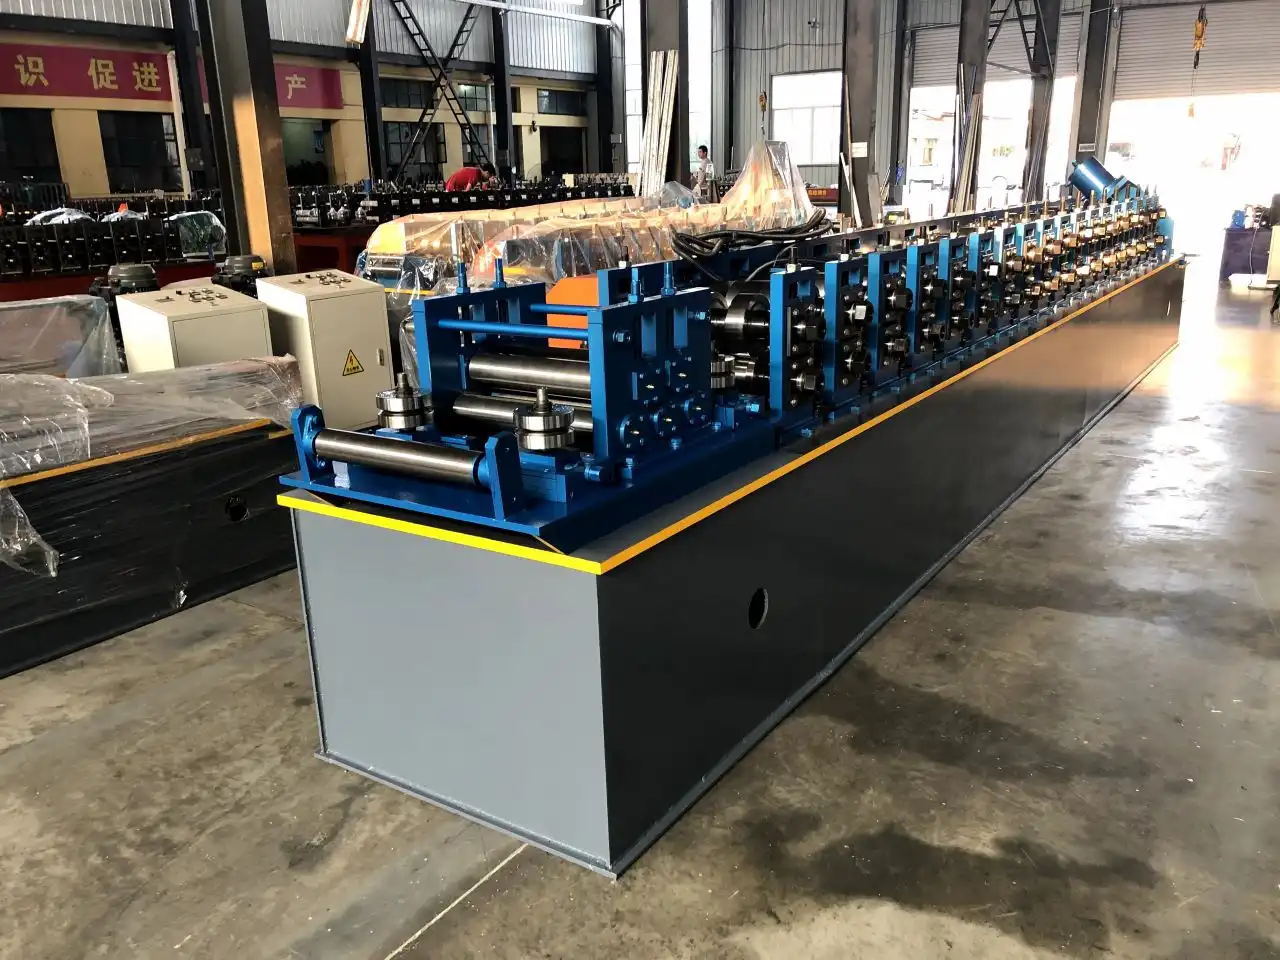
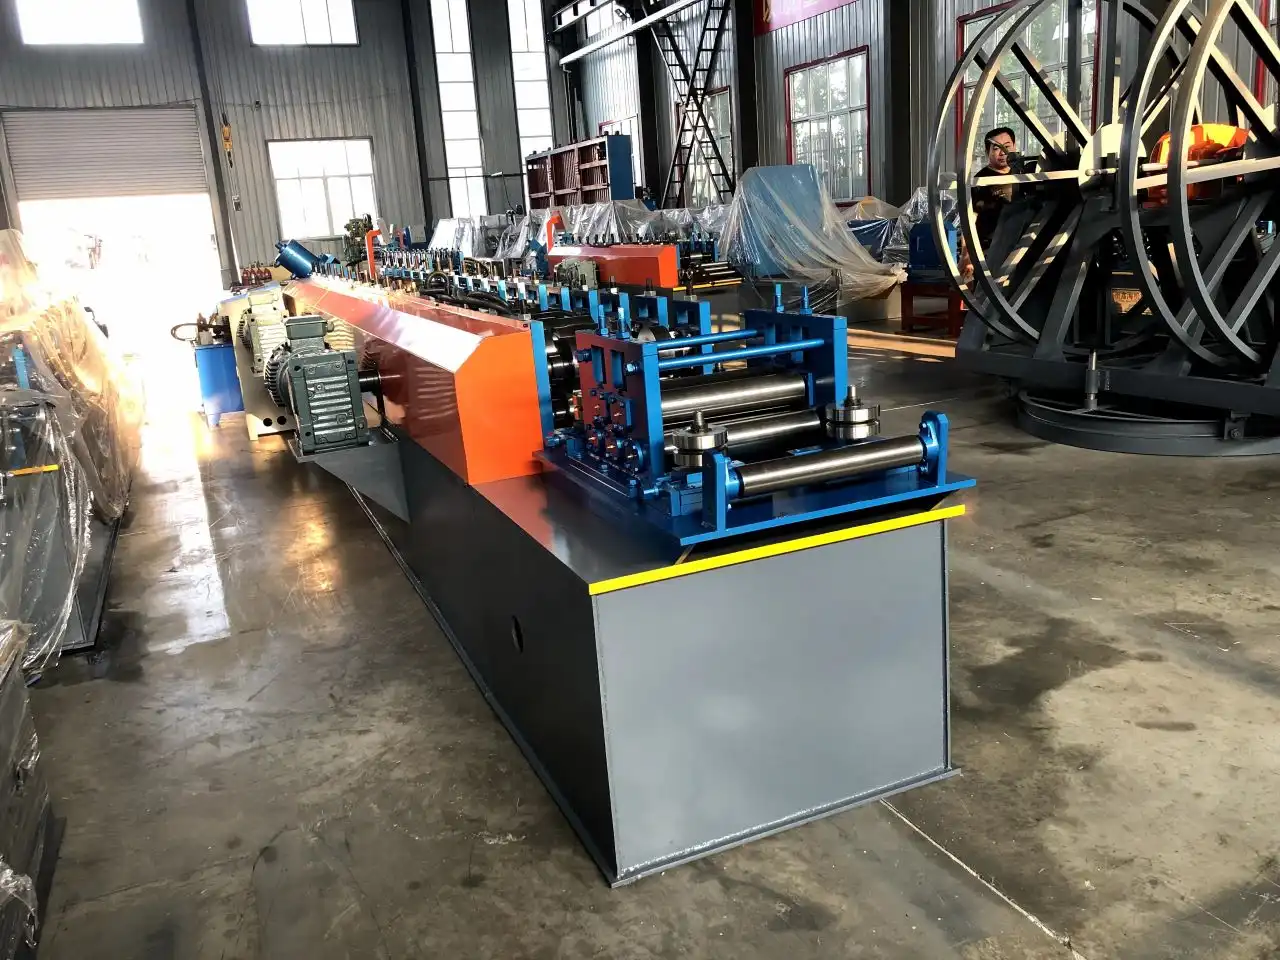
Roll forming is a continuous process in which a flat coil of steel is fed through a succession of roller stations that progressively bend the metal until the final shape (such as a door frame jamb or head section) leaves the line at a constant pace. Forming speeds may be obtained up to 15-25 meters per minute. The procedure is a continual one, so once the line is started, the operator does not have to do anything.
How Hydraulic Press Forming Works
In a hydraulic press, a ram is forced down by pressurized fluid against a die. This bends a steel sheet into a specified form. Each press stroke is a different movement. It does a good job on thick, heavy-gauge material. But each item has to be carried, handled, and cycled individually, which takes longer on big runs.
Where Each Technology Applies in Frame Manufacturing
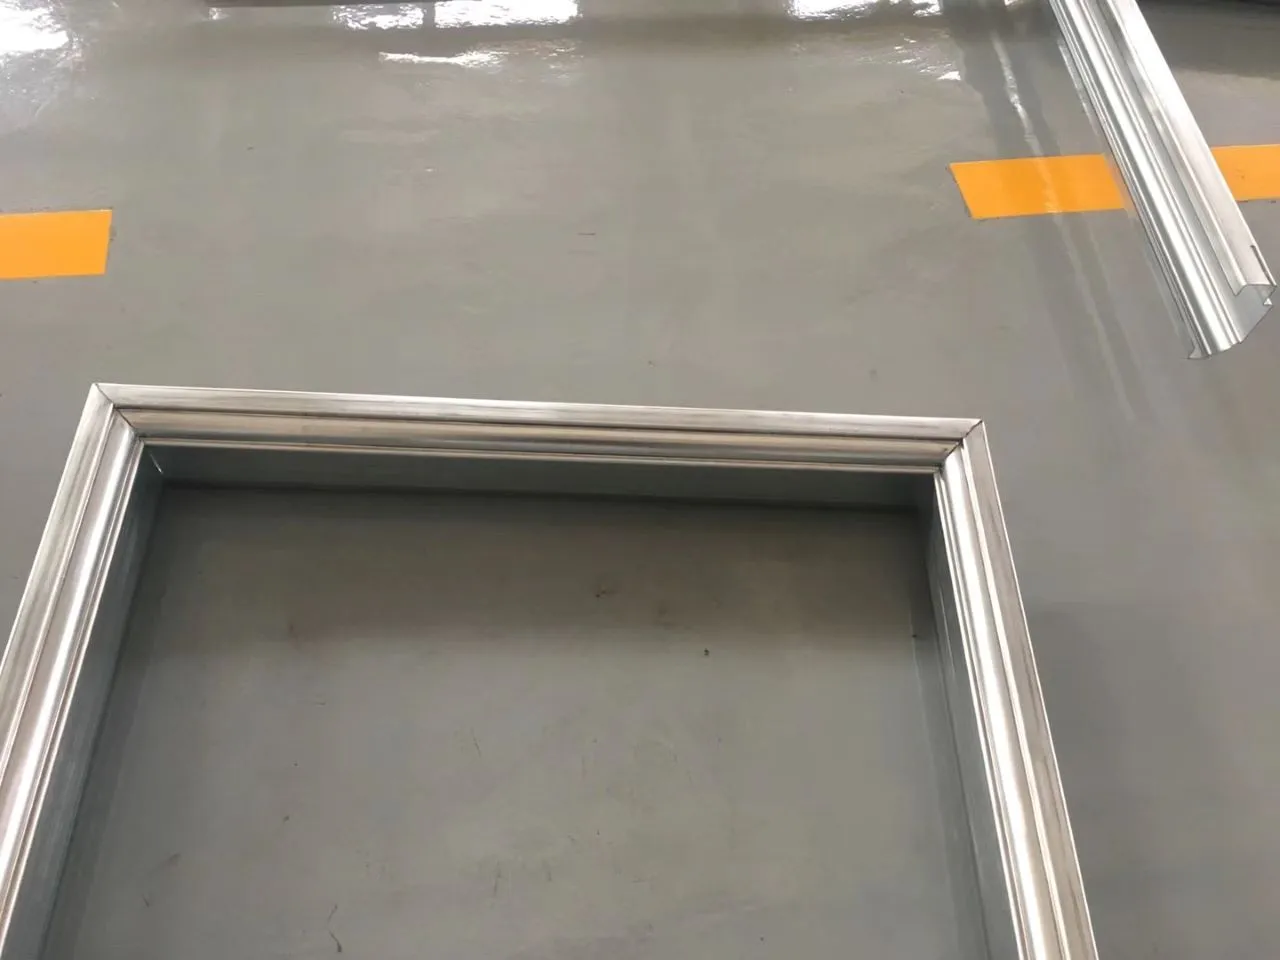
Roll forming is also well suited for long flat parts such as door frame jambs, sills, and knock-down frames for constructed structures. Hydraulic presses are better suited for short-run pressed items, intricate localized features, or heavy-gauge security door supports. The profile body is roll-formed, and a hydraulic press is utilized to punch hinge holes, lock strikes, and miter joints directly on numerous manufacturing lines.
Cost Breakdown: Roll Forming vs Hydraulic Press
This is where the choice becomes real. It's easy to see the differences between these three sets of costs.
Preu de compra inicial
For a hydraulic press, you may buy a simple press brake for about $15,000 USD. However, a custom-constructed cold roll forming line for door frames might cost anywhere from $30,000 to $80,000, depending on the intricacy of the tooling and amount of automation. That seems like a wide gap at first, but it narrows rapidly as output increases.
Costos operatius i consum d'energia
Roll-forming màquina de marc de portas are constantly powered, but their maximum loads are lower. The energy consumption increases with every ram stroke when a lot of weight is involved in the operation of hydraulic presses. Machine manufacturers and industry norms data indicate that hydraulic press systems consume 30-50% more power per unit of output than comparable roll producing lines at the same production rates. Long-term costs include replacement of oil and seals, repairs to pumps and other sections of hydraulic systems.
Total Cost of Ownership Over the Machine Lifecycle
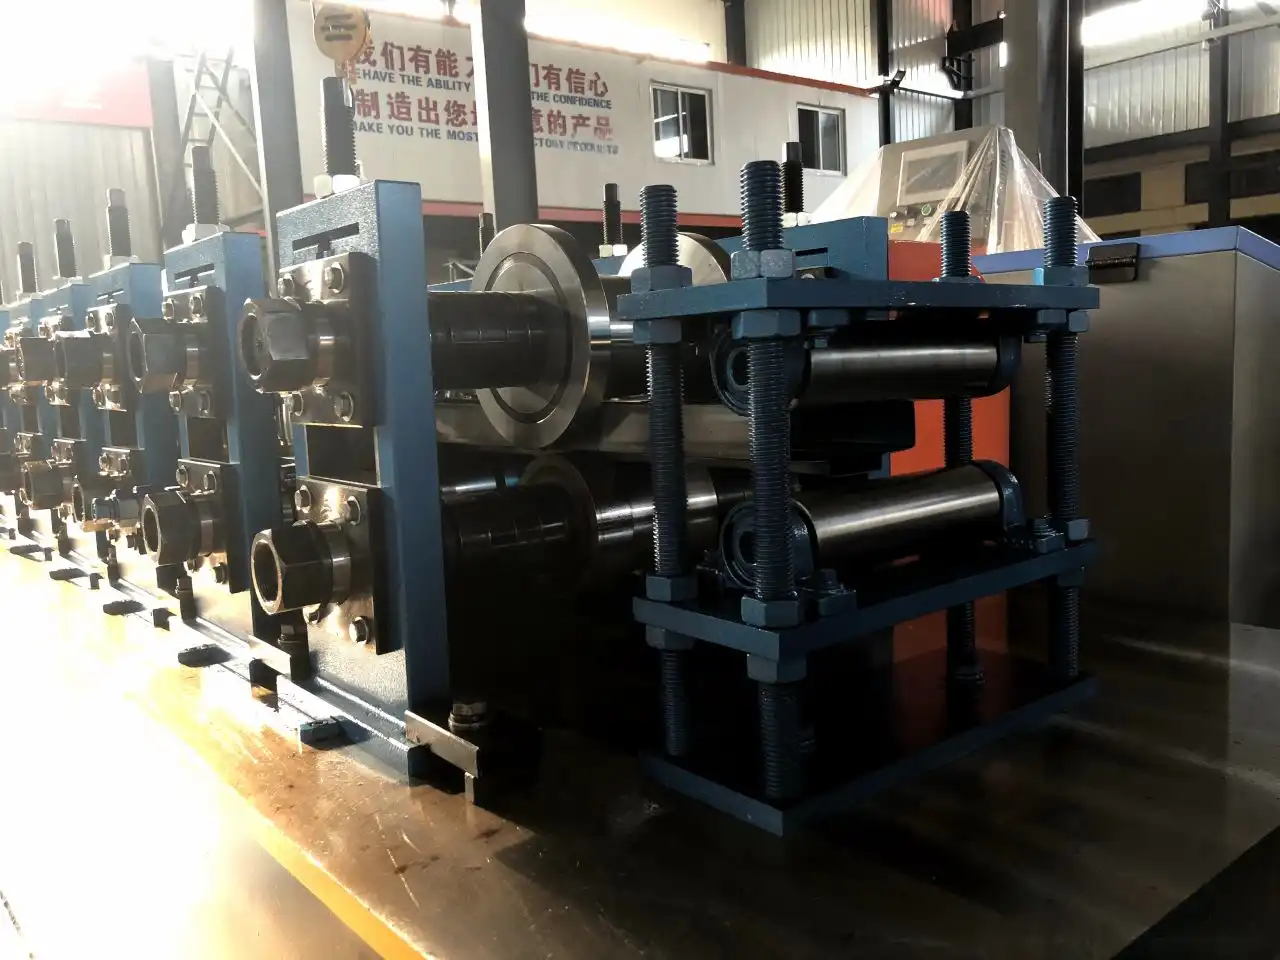
The price paid for an item is not the same as the total cost of ownership (TCO) over 10 years. Roll manufacturing lines, particularly those using GCr15 or Cr12Mov steel rollers hardened to HRC 58-62, repeatedly do the same amount of work with little tool wear even after millions of cycles. Hydraulic press dies, however, wear out faster with severe, repetitive operation and often need more frequent replacement. For enterprises with two or three shifts of manufacturing, a substantial TCO advantage begins to emerge after 18 to 24 months of operation.
Performance and Productivity Impact on Cost Efficiency
Cost efficiency isn't just about the machine price — it's about what the machine produces per hour, per day, and per dollar spent on labor.
Throughput Speed and Output Volume
A roll forming line running at 20 meters per minute produces roughly 1,200 meters of finished door frame profile per hour. A hydraulic press handling individual frame sections might process 40–80 pieces per hour depending on the cycle time and part size. At scale, roll forming's continuous output directly reduces the per-unit labor cost because one operator can supervise the entire line rather than manually feed each press stroke.
Dimensional Accuracy and Scrap Rate
Profile accuracy is non-negotiable in door frame manufacturing, especially for fire-rated and security applications where gap tolerances must stay within tight specifications. Cold roll forming maintains profile cross-section accuracy within ±0.5mm and longitudinal length accuracy within ±1.0mm per 6-meter section. This level of consistency reduces scrap rates and rejected frames — a real cost that many buyers underestimate when comparing machines on price alone.
Automation and Labor Cost Implications
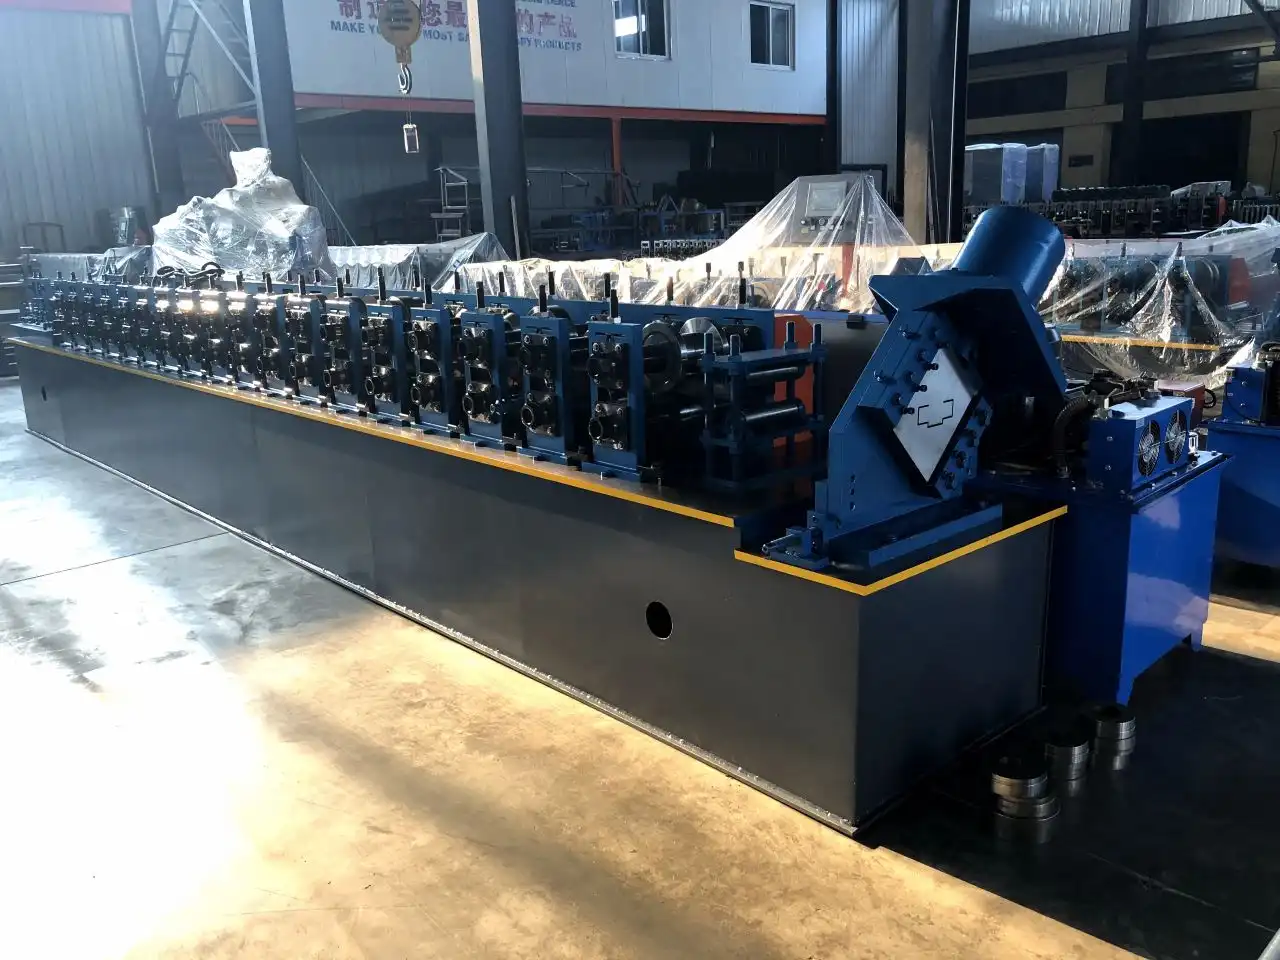
Modern roll forming systems for metal door frames integrate PLC-controlled punching stations, automatic cut-to-length, and even automated stacking. This means one trained operator can run what previously required three or four workers at a press brake station. The labor savings alone can recover the higher upfront door frame machine cost within the first year for factories producing at commercial scale.
Decision-Making Guide: Choosing the Right Machine for Your Business
Which technology sounds more advanced doesn't matter; what matters is how you make music.
Matching Machine Type to Production Volume
For low volume or highly specialized manufacturing, such as creating security màquina de marc de portas one at a time, a hydraulic press may still be a suitable solution, as it is inexpensive to set up and offers more cutting possibilities. But if you are producing 500 or more door frames per day or are involved in large construction or prefab projects, a roll forming process will pay for itself much quicker and keep prices down per unit over time.
Manual vs. Automatic and Stationary vs. Portable
The manual hydraulic press stations take up more floor area per unit of production, and the quality of the output is very much dependent on the expertise of the operator. Automatic roll manufacturing lines, such as compact cassette-type ones, that allow for fast profile changing, reduce setup time from hours to less than thirty minutes. If space is an issue for the factory, there are providers who offer tiny roll forming lines that take up less floor area than a complete press brake configuration.
Eficiència energètica i compliment normatiu
U.S. firms are under increasing pressure to reduce energy usage, both because it is cheaper to do so and because the government wants them to. Roll manufacturing has a lower peak energy consumption, which is more consistent with energy economy objectives. It costs industries more than their power bill to achieve ISO 14001 environmental certification or to comply with state energy laws.
Procurement Insights: Where and How to Buy Door Frame Machines
Buying the right machine at the right price requires more than comparing spec sheets.
Identificació de fabricants i proveïdors fiables
Be sure to choose door frame machine suppliers that can provide proof of ISO 9001 certification, CE compliance, and a history of exports. Machines destined for regulated markets such as the United States and Europe need compliance with certain electrical safety requirements — frequently requiring Siemens or Mitsubishi PLC integration and approved wiring. It is simpler to deal with suppliers in the long term who give detailed documentation including electrical schematics, roller flower drawings, and spare parts lists.
New, Used, and Custom Machine Options
New equipment comes with full warranty coverage and is designed to current standards, while secondhand equipment might provide cost reductions for purchasers with smaller beginning budgets. Manufacturers get a competitive advantage in profile accuracy and production speed with custom roll forming machines, tailored for a particular door frame profile. Make sure to always request a factory acceptance test (FAT) prior to shipping and check that replacement rollers and worn parts are available locally or with acceptable lead times.
Suport postvenda i disponibilitat de peces de recanvi
If assistance is hard to get, the best computer will depreciate fast. Ensure your provider offers remote technical help, video-guided troubleshooting, and a clear replacement parts supply policy. Downtime on a manufacturing line is never free, and even one missed shift might cost more than the price difference between two competing machines.
Conclusió
The cheapest approach to get manymàquina de marc de portas to appear the same is to build them in rolls. Hydraulic presses are still good for heavy-gauge or very specialized work in the short term. When the production level is over a specific level each day, roll forming is a preferable alternative for most commercial door frame producers in the U.S. market. That is because it requires less energy, creates less waste, and can be automated. All of these things cut the true cost per unit over time. But you also want to ensure the technology you choose matches your manufacturing demands, not simply your budget.
FAQ
1. Which technology is better for fire-rated door frame production?
Roll forming is generally preferred for fire-rated door frame production. It maintains the tight gap tolerances required for intumescent seal performance and produces consistent profiles across long runs. For certified fire door manufacturing, dimensional consistency is not optional — it directly affects fire rating test results.
2. What are the typical maintenance challenges with hydraulic press machines?
Hydraulic systems require regular oil changes, seal inspections, and pump servicing. Oil contamination and seal wear are the most common failure points. These maintenance needs translate into recurring costs and potential unplanned downtime that affect production schedules.
3. Can I upgrade from a manual press setup to an automatic roll forming line?
Yes. Many manufacturers make this transition as production volume grows. Suppliers like ZTRFM offer consultations to help factories plan the transition, including profile analysis, tooling design, and line layout planning to fit existing floor space.
4. How precise is cut-to-length on a roll forming line?
High-quality systems maintain accumulated length error within ±1.0mm over a 6-meter section, which meets the requirements for standard door frame installation and fire-rated applications.
5. What material thicknesses can a door frame roll forming machine handle?
Standard machines process material from 0.8mm to 2.0mm thickness, covering most galvanized steel, cold-rolled steel, and light stainless steel applications used in commercial and residential door frame production.
Get a Direct Quote from ZTRFM — Door Frame Machine Manufacturer
Since 2014, ZTRFM has sold cold roll forming equipment to companies in more than 150 countries. Every màquina de marc de porta we make is backed by ISO 9001, CE, and CAS certificacions. Our engineering team can help you choose the right equipment for your production volume and budget, whether you need a standard door frame roll forming line or a custom profile solution. To get a quote or set up a live equipment demonstration, email us at zhongtuorollforming@gmail.com.
referències
1. Halmos, George T. Manual de perfilat. CRC Press, 2006.
2. Schuler GmbH. Manual de conformació de metalls. Springer, 1998.
3. The Fabricator. "Understanding Total Cost of Ownership in Metal Forming Equipment." The Fabricator, 2021.
4. Doors & Hardware Magazine. "Fire Door Frame Tolerances and Certification Requirements." Doors & Hardware, 2022.
5. Modern Metals. "Comparing Roll Forming and Press Brake Operations for High-Volume Production." Modern Metals, 2020.
6. Sheet Metal Industries. "Energy Consumption Benchmarks in Cold Roll Forming vs. Hydraulic Press Operations." Sheet Metal Industries, 2019.